Welcome to our company
Leave Your Message
The global pet food packaging market has experienced unprecedented growth over the past decade, with vacuum packaging emerging as the gold standard for premium pet food products. As pet owners increasingly treat their animals as family members, the demand for high-quality, nutritionally preserved pet food has skyrocketed. Vacuum packaging technology has become instrumental in meeting these elevated expectations, providing superior protection against oxidation, moisture, and contamination while extending shelf life significantly.
The pet food industry is currently valued at over $100 billion globally, with packaging representing approximately 15-20% of total production costs. Vacuum packaging, specifically, has captured a growing market share due to its proven ability to maintain nutritional integrity, preserve flavor profiles, and prevent the degradation of sensitive ingredients such as omega-3 fatty acids, vitamins, and probiotics. Modern vacuum pack solutions incorporate multi-layer barrier films that combine polyethylene, nylon, and metallized layers to create an impermeable shield against oxygen transmission rates (OTR) as low as 0.5 cc/m²/24hrs.
Industry Insight: According to recent market research, the vacuum packaging segment in pet food is projected to grow at a CAGR of 6.8% through 2030, driven by premiumization trends and increased awareness of food safety standards among pet owners.
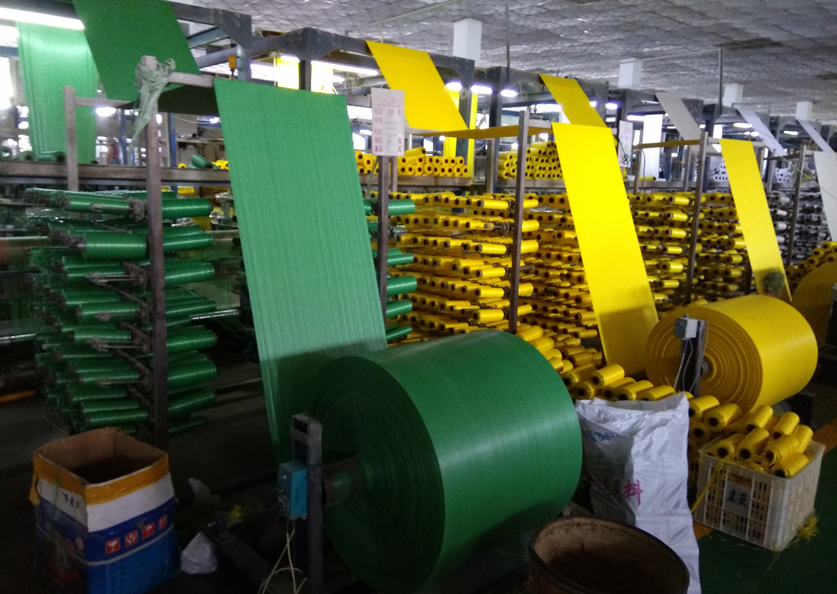
Advanced multi-layer films reduce oxygen transmission to near-zero levels, preventing lipid oxidation and rancidity.
Superior moisture vapor transmission rate (MVTR) control maintains optimal product texture and prevents mold growth.
Vacuum sealing can extend pet food shelf life by 300-500% compared to conventional packaging methods.
The science behind vacuum packaging lies in its ability to create an anaerobic environment that inhibits the growth of aerobic bacteria and molds while dramatically slowing oxidative reactions. For pet food manufacturers, this translates to reduced preservative requirements, maintained nutritional value, and enhanced product appeal. Modern vacuum packaging systems can achieve residual oxygen levels below 2%, which is critical for products containing high-fat content ingredients like salmon oil or chicken fat.
Furthermore, vacuum packaging provides exceptional protection for freeze-dried and dehydrated pet foods, which are particularly susceptible to moisture reabsorption. The hermetic seal created by vacuum technology ensures that these premium products maintain their intended moisture content throughout their shelf life, preserving both texture and nutritional density.
Contemporary vacuum packaging for pet food utilizes sophisticated multi-layer laminate structures, typically consisting of 7-9 layers. These structures commonly include:
These material combinations achieve oxygen transmission rates (OTR) as low as 0.3 cc/m²/24hrs and water vapor transmission rates (WVTR) below 0.5 g/m²/24hrs, providing unparalleled protection for sensitive pet food formulations.
The pet food packaging industry is undergoing a significant transformation toward sustainability. Modern vacuum packaging solutions now incorporate:
These innovations address the growing consumer demand for environmentally responsible packaging while maintaining the stringent performance requirements of pet food preservation.
Vacuum packaging technology serves diverse segments within the pet food industry, each with unique requirements and challenges:
High-end dry pet food formulations containing fresh meat ingredients, probiotics, and omega-rich oils benefit significantly from vacuum packaging. The technology prevents fat oxidation that causes rancidity and preserves the viability of live probiotic cultures. Market data indicates that premium kibble packaged in vacuum-sealed formats commands price premiums of 25-40% over conventionally packaged alternatives, reflecting consumer willingness to pay for perceived quality and freshness.
The rapidly growing raw and freeze-dried pet food segment relies almost exclusively on vacuum packaging technology. These products, which can retail for $8-15 per pound, require absolute moisture and oxygen control to maintain product integrity. Vacuum packaging prevents ice crystal formation in frozen products and moisture reabsorption in freeze-dried formulations, ensuring optimal rehydration characteristics and palatability.
Single-ingredient treats, dental chews, and nutritional supplements represent a $12 billion segment where vacuum packaging provides distinct advantages. The technology preserves volatile flavor compounds, prevents moisture migration, and protects sensitive ingredients like glucosamine and chondroitin from degradation. Vacuum-sealed treat products demonstrate shelf life extensions of 12-18 months compared to 6-9 months for conventionally packaged alternatives.
Market Trend: The humanization of pets continues to drive demand for packaging that mirrors human food standards. Vacuum packaging, long established in human food preservation, benefits from positive consumer associations with quality and freshness.
Professional pet food packaging must navigate a complex regulatory landscape that varies significantly across international markets. Vacuum packaging solutions must comply with:
The U.S. Food and Drug Administration requires that all materials in contact with pet food meet food-contact substance (FCS) regulations under 21 CFR. Vacuum packaging films must demonstrate:
European markets impose stringent requirements under Regulation (EC) No 1935/2004:
Beyond regulatory compliance, quality certifications such as ISO 9001, BRC Global Standards, and FSSC 22000 have become essential for suppliers serving major pet food manufacturers. These certifications demonstrate systematic approaches to quality management, food safety, and continuous improvement.
The vacuum packaging industry for pet food is poised for significant innovation driven by technological advancement and changing consumer expectations:
Next-generation vacuum packaging incorporates intelligent features such as oxygen scavengers, freshness indicators, and time-temperature indicators (TTIs). These active packaging technologies provide real-time feedback on product condition, enabling both manufacturers and consumers to monitor freshness throughout the supply chain. Near-field communication (NFC) tags and QR codes embedded in vacuum packaging enable traceability, authenticity verification, and direct consumer engagement through smartphone integration.
Advanced packaging lines now combine vacuum technology with controlled atmosphere replacement, typically using nitrogen or carbon dioxide gas flushing before final sealing. This hybrid approach, known as vacuum skin packaging (VSP) or compensated vacuum packaging, provides optimal protection for products where complete vacuum compression might damage product structure. The technology is particularly valuable for soft treats and semi-moist pet food products.
Modern vacuum packaging operations increasingly leverage automation, machine learning, and Internet of Things (IoT) connectivity. Automated quality control systems using vision inspection detect seal integrity issues, while predictive maintenance algorithms minimize downtime. Real-time data analytics optimize packaging parameters for different product formulations, ensuring consistent quality while maximizing throughput efficiency.
Innovation Spotlight: Emerging bio-based barrier coatings derived from chitosan and cellulose nanocrystals show promise in replacing synthetic barrier layers while maintaining comparable oxygen barrier performance, potentially revolutionizing sustainable vacuum packaging solutions.
Years of Excellence
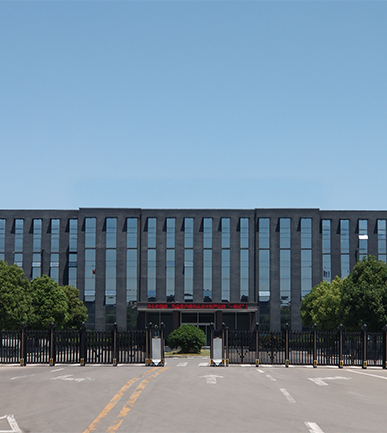
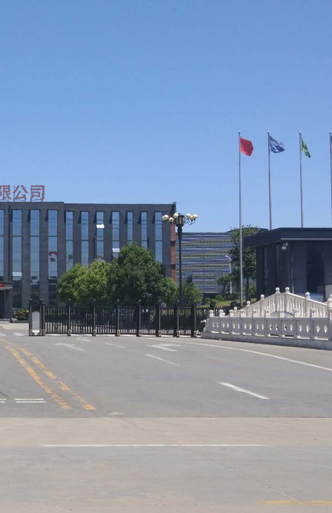
Shandong Jike International Trade Co., Ltd. is a state-owned professional food packaging and printing enterprise, established in 2003 and located in Shandong Province, eastern China. The company has obtained and passed ISO9001, ISO14001, and ISO45001 certifications, and all our products have passed QS food safety certification.
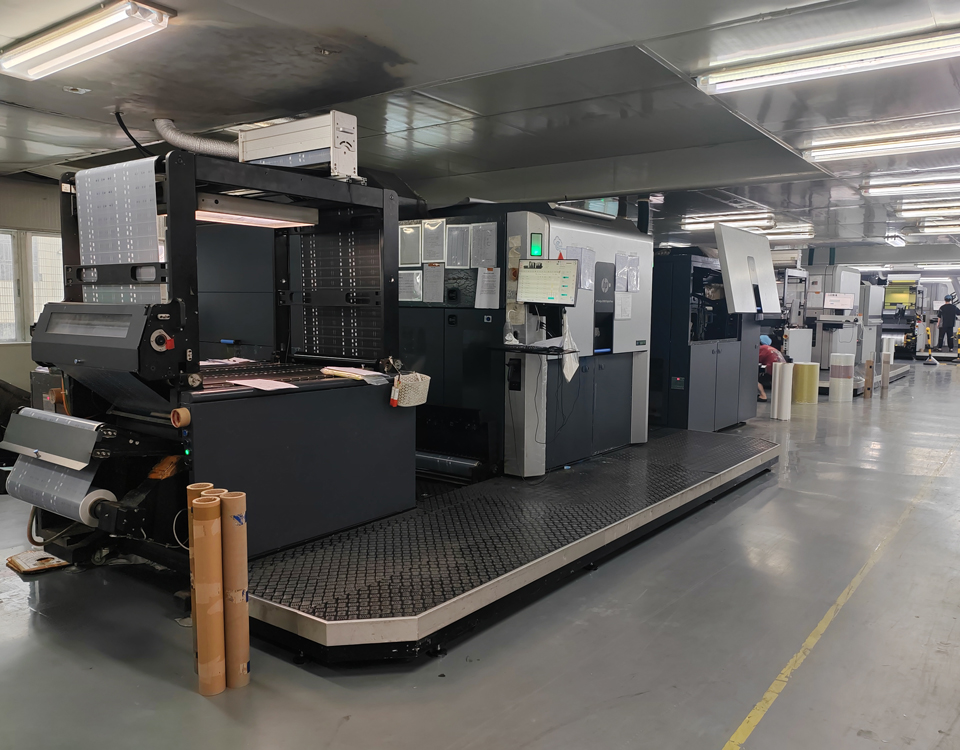
With over two decades of specialized experience in vacuum packaging solutions for the pet food industry, we have developed comprehensive expertise in barrier film technology, custom printing capabilities, and international compliance standards. Our manufacturing facilities employ state-of-the-art gravure printing presses, solventless lamination equipment, and high-speed pouch-making machinery capable of producing over 10 million units monthly.
The company's core export products cover the needs of multiple industries, mainly including food-grade flexible packaging, pet food packaging, polyethylene film, and woven packaging bags, which can accurately match the market standards of different regions such as North America, the European Union, Southeast Asia, and the Middle East.
We also support multi-language design and printing, barcode/QR code customization, material combination selection, and thickness selection to fully meet the needs of cross-border trade. Our vacuum packaging solutions are specifically engineered for pet food applications, offering customizable structures from 80 microns to 200 microns total thickness, with barrier configurations optimized for different product types and shelf life requirements.
In terms of supply chain and service, the company has strong cross-border delivery capabilities. We have standardized production workshops and automated production lines, with flexible minimum order quantities for regular products. We undertake both small-batch customization and large-volume order production.
We have established a strict quality control system, tracing the entire process from raw material procurement and production processing to finished product inspection, ensuring that every batch of products meets the quality standards of the importing country. We are equipped with a professional cross-border logistics team to support various transportation methods such as full container shipping, LCL shipping, and air freight.
Our production capacity includes 15 high-speed vacuum packaging lines with integrated quality control systems, enabling rapid turnaround times of 15-20 days for standard orders and 25-30 days for fully customized solutions including artwork development and pre-production sampling.
Our vacuum packaging solutions have been adopted by leading pet food manufacturers across multiple continents, supporting product launches in premium, natural, and specialty diet categories. Representative partnerships include:
Collaboration with top-tier pet food brands requiring ultra-high barrier packaging for grain-free and raw-inspired formulations.
Supporting clean-label brands with sustainable packaging solutions that maintain product integrity without synthetic preservatives.
Providing customized packaging for veterinary diets, limited-ingredient formulas, and functional pet foods with specific nutritional targets.
Case studies demonstrate that our vacuum packaging solutions have enabled clients to achieve shelf life extensions of 40-60% compared to previous packaging formats, reduce product returns due to freshness complaints by over 75%, and successfully enter new international markets with confidence in product quality maintenance throughout extended distribution chains.
Since its establishment 23 years ago, relying on excellent product quality, comprehensive compliance guarantees, and efficient cross-border services, Jike Packaging Printing has established long-term cooperative relationships with customers in more than 50 countries and regions worldwide, serving clients including globally renowned food manufacturers, brand owners, and trading companies. In the future, we will continue to focus on changes in international market demand, using innovative technology and high-quality services as a link to become a trusted cross-border flexible packaging printing partner for global customers.
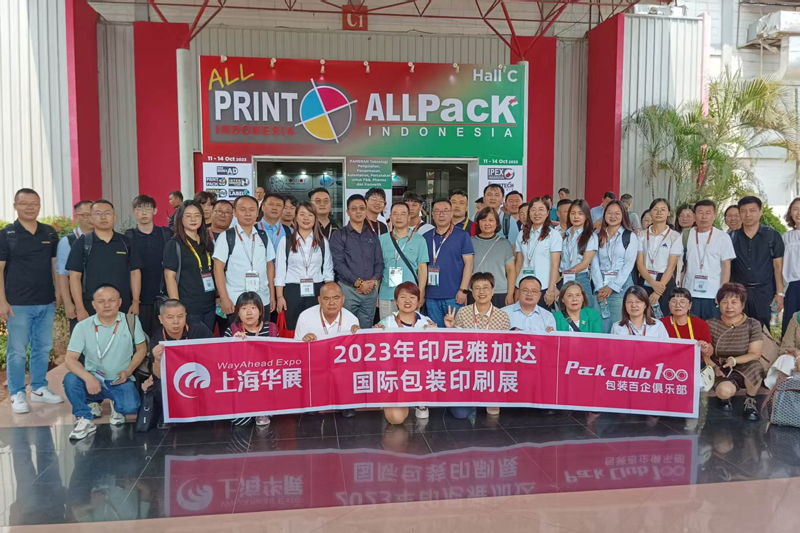
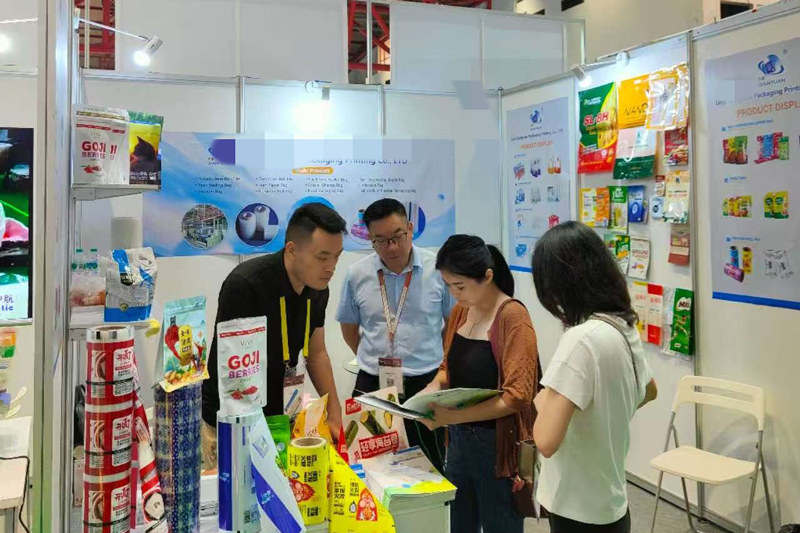
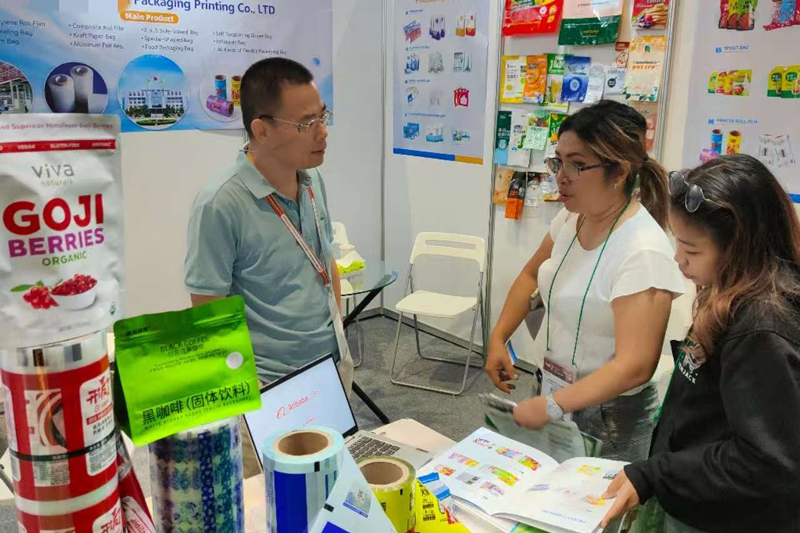
We actively participate in major international packaging and pet food trade shows, demonstrating our commitment to industry engagement and continuous innovation. Our presence at events such as Petfood Forum, GlobalPETS Forum, and Pack Expo provides opportunities for direct collaboration with industry leaders and emerging brands.
Vacuum packaging technology represents the convergence of material science, food safety, and consumer expectations in the professional pet food industry. As the market continues to evolve toward premium, natural, and specialized nutrition products, the role of advanced packaging becomes increasingly critical. The ability to preserve nutritional integrity, extend shelf life without excessive preservatives, and provide visible quality assurance makes vacuum packaging an indispensable tool for modern pet food manufacturers.
Looking forward, the integration of sustainable materials, smart packaging features, and enhanced barrier technologies will further solidify vacuum packaging's position as the preferred solution for professional pet food applications. Manufacturers who invest in high-quality vacuum packaging solutions position themselves advantageously in competitive markets where product differentiation and quality perception drive purchasing decisions.
For brands seeking to elevate their product offerings, enter new markets, or extend distribution reach, partnering with experienced vacuum packaging specialists like Shandong Jike International Trade Co., Ltd. provides access to proven technology, regulatory expertise, and manufacturing capabilities essential for success in the global pet food industry.