Welcome to our company
Leave Your Message
Explore our best-selling vacuum pack and resealable liquid pouching products — designed for food, beverage, sauce, and industrial liquid applications worldwide.
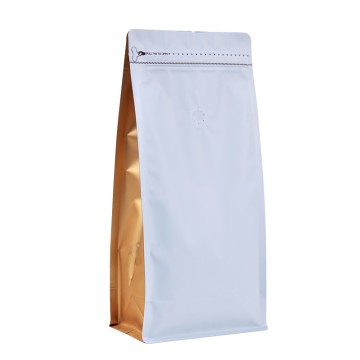
Food-grade high-barrier multi-layer vacuum pack with degassing valve and resealable zipper — ideal for liquid and semi-liquid products.
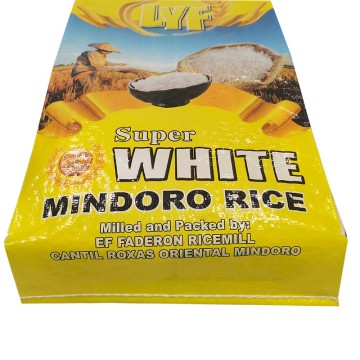
High-strength laminated polypropylene sack engineered for bulk liquid and agricultural packaging applications up to 25kg.
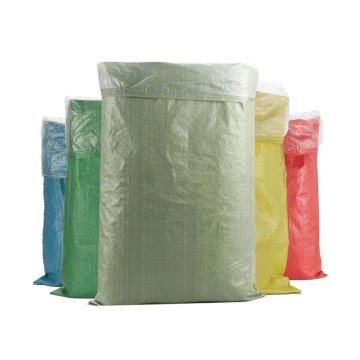
Fully customizable vacuum packaging solutions — design, material, structure, size, and print tailored to your liquid pouching needs.
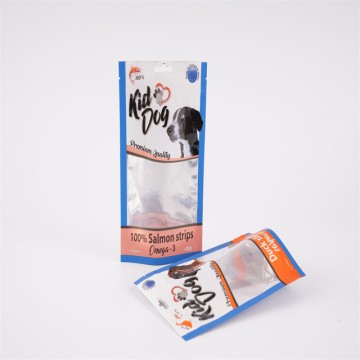
Premium octagonal-side sealed resealable vacuum pouch with stand-up design — perfect for liquid, wet food, and treat packaging.
Vacuum pack technology for liquid pouching represents one of the most significant advancements in flexible packaging over the past two decades. By removing air from within a sealed pouch prior to or during the filling process, vacuum packs dramatically extend the shelf life of liquid contents — whether food-grade beverages, sauces, dairy products, industrial chemicals, or pharmaceutical fluids.
A resealable liquid pouch combines the airtight integrity of vacuum sealing with the consumer convenience of a reopenable closure — typically a zipper lock, spout cap, or press-to-close mechanism. This dual functionality makes vacuum-sealed resealable pouches an indispensable solution across food retail, e-commerce, foodservice, and industrial supply chains.
🔬 Key Insight: The global flexible packaging market is projected to exceed USD 300 billion by 2028, with vacuum-sealed liquid pouches among the fastest-growing segments — driven by consumer demand for freshness, portability, and reduced plastic waste.
The adoption of vacuum pack technology for liquid pouching has accelerated across a diverse range of commercial and industrial sectors. In the food and beverage industry, brands are increasingly replacing rigid glass and plastic containers with lightweight, vacuum-sealed flexible pouches that reduce shipping costs by up to 40% while maintaining superior barrier properties.
In the industrial sector, vacuum liquid pouches are used for packaging lubricants, adhesives, chemical reagents, and cleaning solutions — where precise dosing, contamination prevention, and extended storage stability are critical requirements. The pharmaceutical and nutraceutical industries rely on vacuum-sealed pouches for liquid supplements, IV fluids, and topical formulations where sterility and oxygen exclusion are non-negotiable.
From a commercial standpoint, the shift toward direct-to-consumer (DTC) e-commerce has been a major catalyst. Vacuum-sealed resealable liquid pouches are inherently leakproof, lightweight, and compressible — making them ideal for fulfillment center operations and last-mile delivery where traditional rigid containers frequently fail.
Several macro trends are converging to accelerate growth in the vacuum pack resealable liquid pouch market:
From kitchen to clinic, from factory floor to fulfillment center — vacuum resealable liquid pouches deliver unmatched versatility across industries.
Vacuum-sealed spout pouches for ketchup, soy sauce, salad dressing, and hot sauce maintain flavor integrity and prevent oxidation — with resealable spout caps for portion-controlled dispensing.
From fruit juice to energy drinks and cold-brew coffee, stand-up vacuum liquid pouches with resealable zipper or spout deliver shelf-stable, portable, and visually impactful packaging for retail and foodservice.
Liquid shampoo, lotion, serum, and gel products benefit from vacuum pouches that prevent oxidation and contamination — with resealable closures enabling hygienic multiple-use dispensing.
Sterile vacuum pouches for liquid supplements, oral medications, and topical solutions ensure product integrity, precise dosing, and compliance with GMP and FDA packaging standards.
Solvent-resistant multi-layer vacuum pouches for adhesives, lubricants, and chemical reagents provide leak-proof containment, extended storage stability, and safe handling for industrial supply chains.
Retort-grade vacuum liquid pouches for wet pet food, broths, and liquid animal supplements maintain nutritional value and palatability without preservatives — with resealable closures for multi-serve convenience.
The vacuum resealable liquid pouch industry is at an inflection point, driven by technology, sustainability, and shifting consumer behavior.
Leading manufacturers are transitioning from multi-material laminates to mono-material PE and PP vacuum pouches that maintain barrier performance while achieving full recyclability — aligned with EU Packaging Regulation 2025 and global EPR frameworks.
Machine vision and AI-powered inspection systems are being integrated into vacuum pouch sealing lines to detect micro-leaks, seal defects, and fill-weight deviations in real time — achieving near-zero defect rates at high production speeds.
Embedded NFC tags and printed freshness sensors in vacuum liquid pouches enable consumers to verify product authenticity, check remaining shelf life, and access brand content via smartphone — creating new touchpoints in the liquid packaging journey.
PLA-based and cellulose-derived barrier films are entering commercial production for vacuum liquid pouches — offering compostable end-of-life options for brands targeting zero-waste certifications and environmentally conscious consumers.
New-generation VFFS and pre-made pouch filling machines specifically engineered for vacuum liquid pouches achieve outputs of 80–150 pouches per minute with integrated vacuum pull and reseal verification — enabling scalable production for global brands.
Vacuum resealable liquid pouches are being engineered specifically for air freight and parcel delivery — with enhanced puncture resistance, pressure-differential seals, and leakproof spout designs that withstand the rigors of international e-commerce logistics.
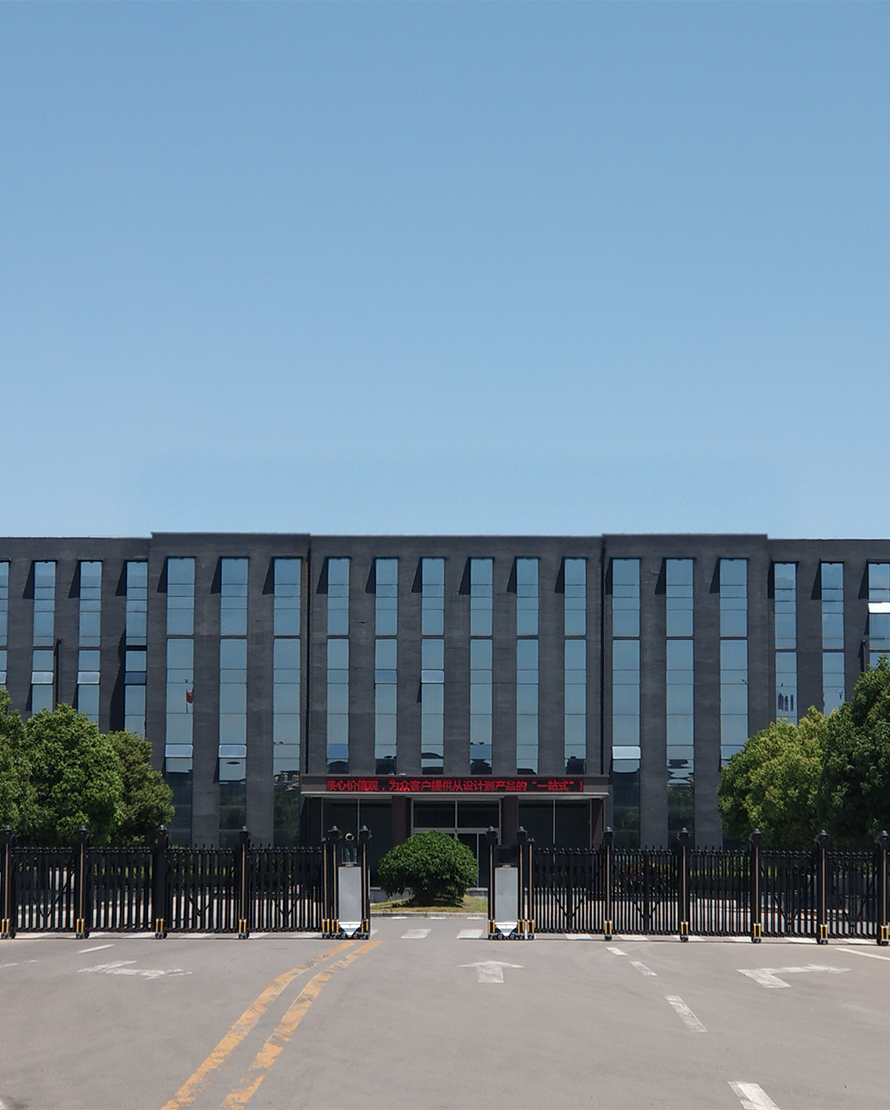
Shandong Jike International Trade Co., Ltd. is a state-owned professional food packaging and printing enterprise, established in 2003 and located in Shandong Province, eastern China. The company has obtained and passed ISO9001, ISO14001, and ISO45001 certifications, and all products have passed QS food safety certification.
As a pioneer in the packaging industry deeply rooted in North China, Jike is one of the premier one-stop providers of food packaging bags, pet packaging bags, vacuum liquid pouches, and woven bags. Since our founding in 2003, we have built upon more than 22 years of profound industry experience to establish a complete value chain — achieving an impressive annual capacity of 5,000 tons of food packaging bags and 3,000 tons of woven bags.
We also support multi-language design and printing, barcode/QR code customization, material combination selection, and thickness selection to fully meet the needs of cross-border trade.
Learn More About UsEvery vacuum resealable liquid pouch undergoes rigorous quality inspection at each stage of production — from raw material selection to final shipment.
Food-grade barrier films and laminates verified for OTR, WVTR, and food safety compliance.
Up to 9-color high-resolution printing with stable color consistency for premium brand presentation.
Multi-layer lamination with controlled curing to achieve target barrier and seal strength properties.
Precision heat-sealing with integrated zipper, spout, and valve assembly for resealable liquid pouches.
Final leak test, visual inspection, and packing — with LCL/FCL and express door-to-door delivery options.

JIKE is a one-stop provider of food packaging bags, vacuum liquid pouches, pet packaging bags, and woven bags — everything you need from a single trusted source.

We customize everything — design, material structure, barrier layers, thickness, zipper type, spout style, size, and printing — to meet any vacuum liquid pouching requirement.

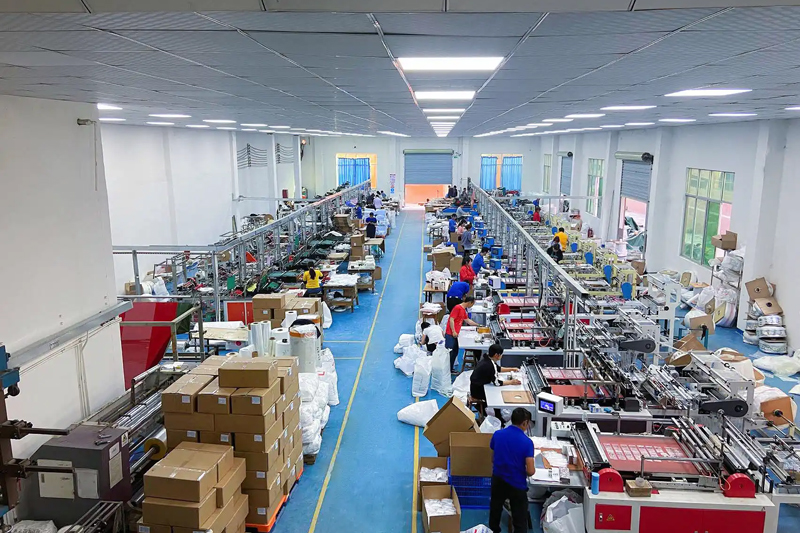
From raw material to color printing, lamination, curing, bag making, and shipment — every step is strictly inspected to ensure your vacuum pack liquid pouches meet the highest standards.

LCL and FCL container delivery, plus DHL/FedEx express for small quantities — seamless door-to-door logistics for vacuum liquid pouch orders to 70+ countries worldwide.
Selecting the optimal vacuum pack laminate structure for liquid pouching is a critical engineering decision that directly impacts product shelf life, consumer experience, and total cost of ownership. The most common multi-layer structures used in liquid vacuum pouches include:
🌟 Pro Tip: For resealable liquid pouches in e-commerce applications, always specify a minimum seal strength of 40 N/15mm and a zipper pull force of 15–25 N to ensure leak-proof performance through the entire fulfillment and delivery cycle.
The resealable closure is the defining feature that differentiates a premium vacuum liquid pouch from a conventional single-use pack. The main closure technologies available include:
The liquid vacuum pouch industry is navigating an increasingly complex regulatory landscape. In the European Union, the Packaging and Packaging Waste Regulation (PPWR) mandates that all packaging placed on the EU market must be recyclable by 2030. In the United States, the FDA's guidance on food contact materials continues to evolve, with growing scrutiny of PFAS-containing barrier coatings in food-grade liquid pouches.
At Jike, all food-grade vacuum liquid pouches are manufactured using materials that comply with GB 9685, EU Regulation 10/2011, and FDA 21 CFR food contact material standards. Our ISO 14001 environmental management certification reflects our commitment to reducing the environmental footprint of our manufacturing operations — including solvent recovery systems, energy-efficient printing presses, and waste minimization programs throughout our production facility in Shandong Province.
From spout pouches and stand-up liquid bags to vacuum-sealed food pouches and woven sacks — Jike offers a comprehensive range of flexible packaging solutions for every liquid pouching application.
Food-grade multi-layer vacuum pouch with degassing valve, resealable zipper, and high-barrier laminate for coffee, tea, and liquid food products.
Heavy-duty laminated polypropylene woven sack for bulk liquid, rice, grain, and agricultural product packaging up to 25kg.
Fully customizable vacuum liquid pouch — design, material, size, print, and closure type tailored to your brand and product specifications.
Premium octagonal-side sealed resealable vacuum stand-up pouch — ideal for liquid pet food, wet treats, and consumer food products.
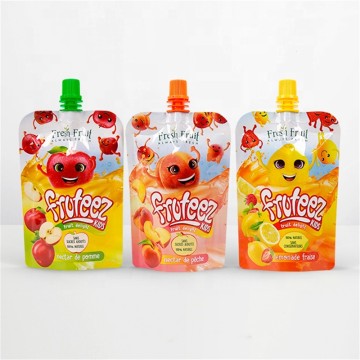
Custom printed stand-up spout pouch for sauce, juice, beverage, and liquid food — with resealable screw-cap spout for drip-free dispensing.
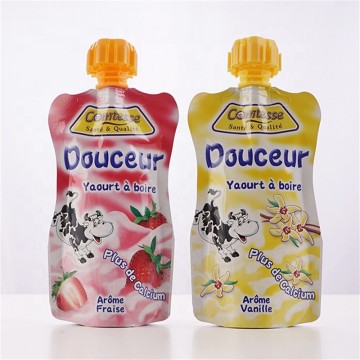
Pre-formed stand-up liquid pouch with integrated spout and valve — available in 100ml, 250ml, 300ml, and 500ml capacities for water, juice, and liquid food.
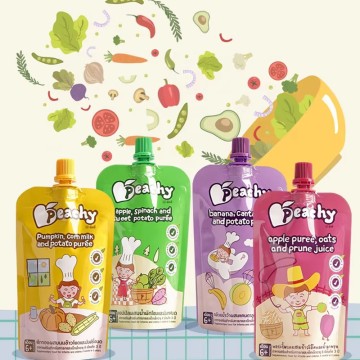
Custom-printed resealable spout pouch with nozzle design for juice, drink, and liquid packaging — featuring suction nozzle for direct consumption convenience.
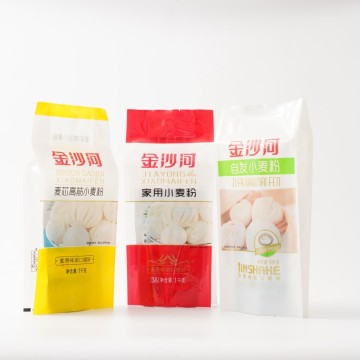
Four-side sealed flat bottom vacuum pouch with carry handle — versatile high-performance packaging for food, liquid, and pharmaceutical products.
Ready to elevate your liquid product packaging with premium vacuum resealable pouches? Contact Jike today for custom samples, competitive quotes, and expert packaging consultation — we reply within 24 hours.
Customize My Own Style
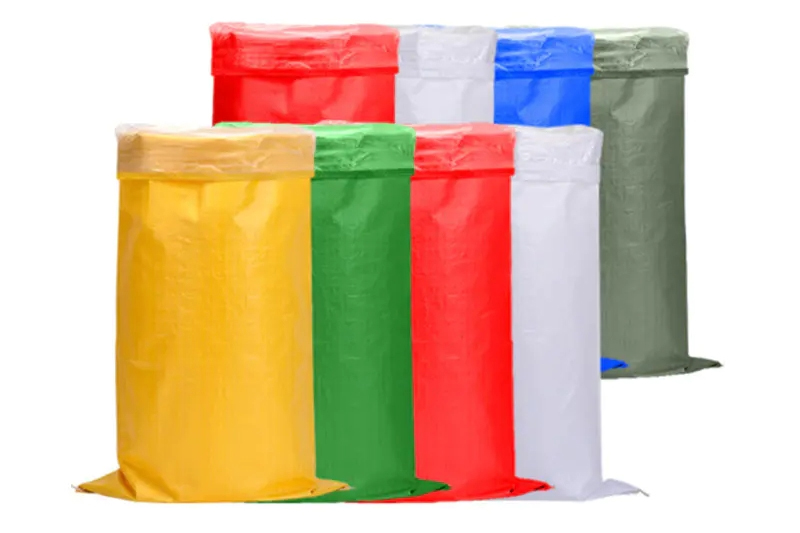
As the global demand for sustainable packaging continues to grow, more and more businesses are turning to innovative polypropylene-based solutions to reduce environmental impact while maintaining performance.

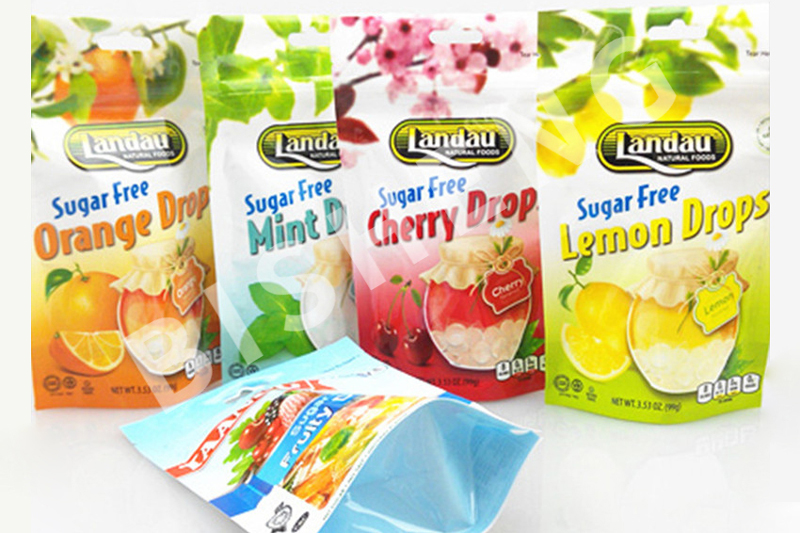
Stand-up bags — also known as doypack pouches — are becoming increasingly popular in the liquid packaging industry due to their shelf appeal, space efficiency, and consumer convenience.
Entering 2026 and beyond, vacuum pack and liquid pouching trends will reflect broader shifts in sustainability, smart packaging technology, and global e-commerce logistics requirements.