Welcome to our company
Leave Your Message
Explore our premium grade, high-barrier sealed food bags engineered specifically for long-term freshness and industrial distribution.
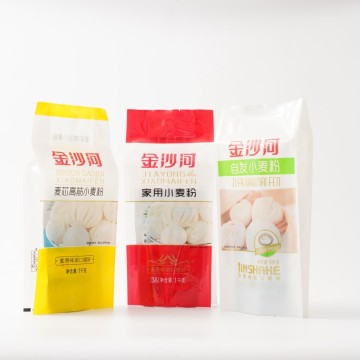
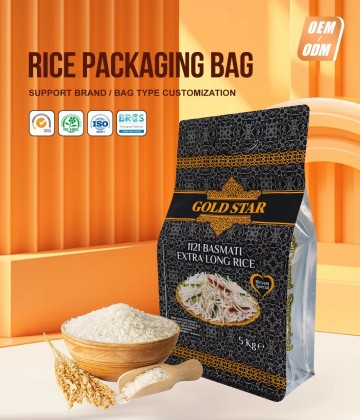
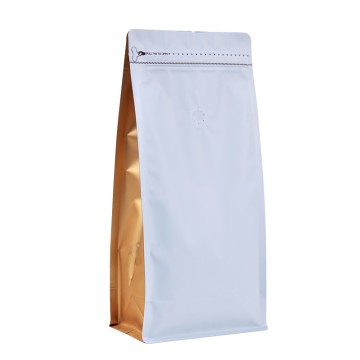
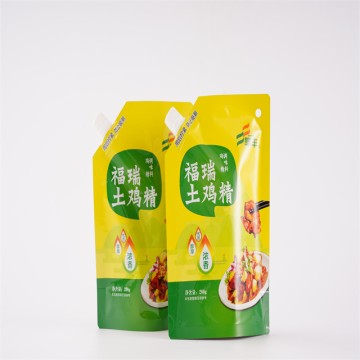
In the modern globalized food supply chain, food preservation is no longer just about preventing immediate spoilage; it is a critical driver of economic efficiency, sustainability, and food security. The utilization of a specialized sealed food bag for long-term vacuum food storage represents one of the most significant technological advancements in flexible packaging. By extracting atmospheric oxygen and hermetically sealing the contents, these packaging systems inhibit aerobic bacterial growth, prevent lipid oxidation, eliminate moisture ingress, and dramatically extend product shelf life.
Globally, commercial food processors, agricultural exporters, and retail brands are transitioning rapidly from rigid containers to flexible, high-barrier vacuum bags. This paradigm shift is driven by the necessity to reduce transportation costs—since flexible packaging is significantly lighter and takes up less volume than metal cans or glass jars—and to meet stringent international food safety standards. The market value for vacuum packaging bags is experiencing a robust compound annual growth rate (CAGR), fueled by the booming ready-to-eat meal industry, premium coffee exports, pet food manufacturing, and bulk grain logistics.
Traditional single-layer plastics are highly permeable to oxygen and moisture, making them entirely unsuitable for long-term vacuum storage. Today's industrial-grade sealed food bags utilize sophisticated multi-layer co-extrusion technology. By bonding multiple polymer layers—such as Oriented Polyamide (OPA/Nylon) for mechanical strength and puncture resistance, Ethylene Vinyl Alcohol (EVOH) as an ultra-high oxygen barrier, and Polyethylene (PE) as a reliable, food-safe heat-sealing layer—manufacturers can customize the Oxygen Transmission Rate (OTR) and Water Vapor Transmission Rate (WVTR) to match the exact biological requirements of the food product.
Years of Production Experience
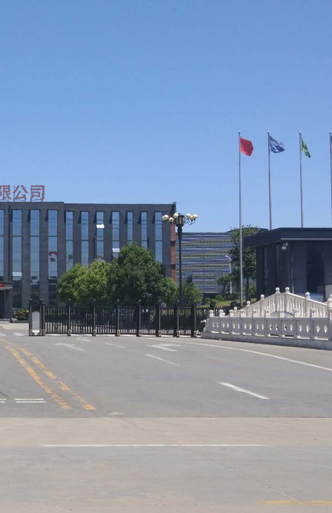
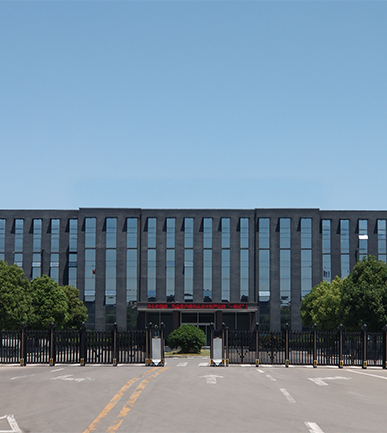
Shandong Jike International Trade Co., Ltd. is a state-owned professional food packaging and printing enterprise, established in 2003 and located in Shandong Province, eastern China. The company has obtained and passed ISO9001, ISO14001, and ISO45001 certifications, and all our products have passed QS food safety certification.
With a foundation built on precision manufacturing and rigorous quality control, we have evolved from a regional supplier into a prominent global player in the flexible packaging sector. Our state-of-the-art facility features high-speed rotogravure printing presses, solvent-free lamination machines, and advanced pouch-making equipment, enabling us to deliver premium-grade vacuum bags that meet the strict regulatory requirements of global food industries.
Welcome to learn about our company. The company's core export products cover the needs of multiple industries, mainly including food-grade flexible packaging, pet food packaging, polyethylene film, and woven packaging bags, which can accurately match the market standards of different regions such as North America, the European Union, Southeast Asia, and the Middle East. We also support multi-language design and printing, barcode/QR code customization, material combination selection, and thickness selection to fully meet the needs of cross-border trade.
In terms of supply chain and service, the company has strong cross-border delivery capabilities. We have standardized production workshops and automated production lines, with flexible minimum order quantities for regular products. We undertake both small-batch customization and large-volume order production; we have established a strict quality control system, tracing the entire process from raw material procurement and production processing to finished product inspection, ensuring that every batch of products meets the quality standards of the importing country; and we are equipped with a professional cross-border logistics team to support various transportation methods such as full container shipping, LCL shipping, and air freight.
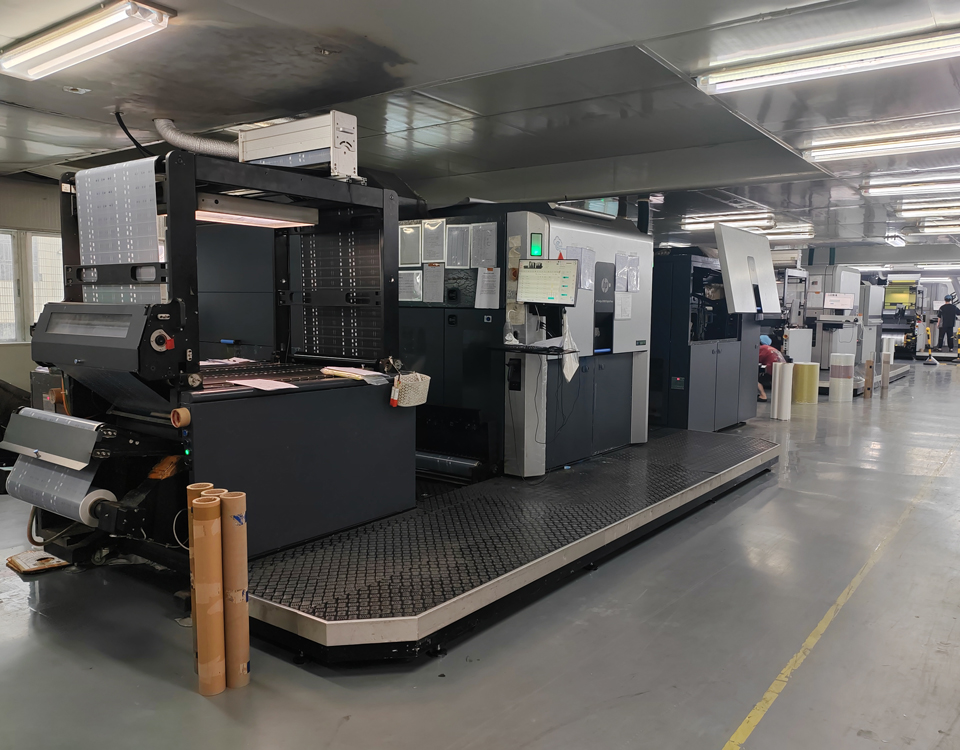
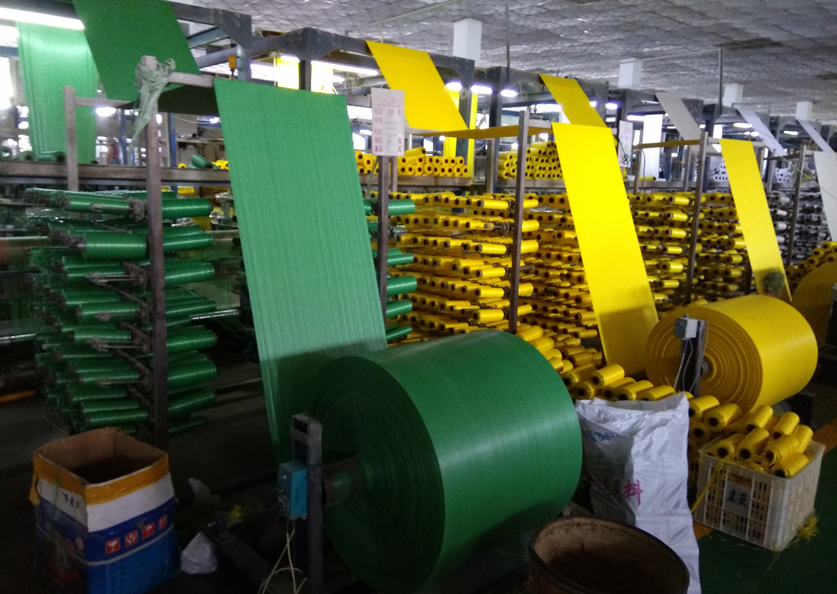
In terms of supply chain and service, the company has strong cross-border delivery capabilities. We have standardized production workshops and automated production lines, with flexible minimum order quantities for regular products. We undertake both small-batch customization and large-volume order production; we have established a strict quality control system, tracing the entire process from raw material procurement and production processing to finished product inspection, ensuring that every batch of products meets the quality standards of the importing country; and we are equipped with a professional cross-border logistics team to support various transportation methods such as full container shipping, LCL shipping, and air freight.
Our strategic location in Shandong allows us direct access to major international shipping ports, minimizing transit times and optimizing shipping routes. Whether you require custom-printed stand-up pouches for retail or heavy-duty flat bottom bags for industrial raw materials, our dedicated logistics specialists coordinate the entire export process, handling customs documentation, compliance verification, and tracking to ensure seamless door-to-door delivery.
From agricultural fields to high-tech retail environments, vacuum packaging plays a versatile role in maintaining quality and extending shelf life.
In large-scale agricultural trade, grains are highly susceptible to moisture, mold, and insect infestations. Using a heavy-duty, heat-sealed vacuum bag constructed from multi-layer PA/PE co-extruded film ensures that grains like rice and oats remain in an oxygen-deprived environment. This prevents the germination of insect larvae and inhibits mold development, keeping the grains fresh and nutritionally intact for up to several years. Flat-bottom bag designs with integrated handles facilitate efficient stacking in warehouses and retail displays alike.
Coffee beans are highly sensitive to oxygen, light, and humidity. Once roasted, they begin to release carbon dioxide and lose their complex volatile aromatic compounds. To counter this, advanced coffee packaging utilizes an 8-side sealed flat bottom bag equipped with a one-way degassing valve. This valve allows the escaping CO2 to exit the bag without letting external oxygen enter, preserving the pristine flavor profile of the coffee beans for extended periods, making it ideal for international export and long-term shelf display.
For fresh meats, seafood, and processed proteins like beef jerky, vacuum packaging is indispensable. By removing oxygen, the growth of aerobic bacteria is halted, which is the primary cause of meat spoilage. In addition, vacuum-sealed bags protect proteins from freezer burn when stored in low-temperature warehouses. The high-puncture-resistance polymer layers prevent bones or hard spices from tearing the film, maintaining the hermetic seal throughout the logistics cycle.
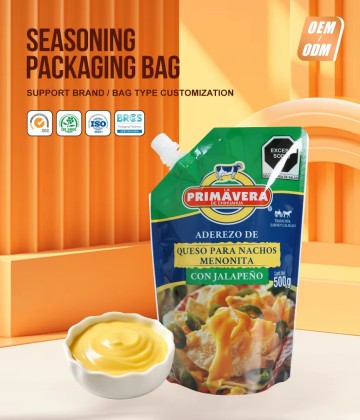
The transport of liquids, purees, and sauces has traditionally relied on heavy, breakable glass jars or rigid cans. Today, high-barrier stand-up pouches with integrated spouts offer a lightweight, puncture-resistant alternative. These pouches are vacuum-filled to eliminate head-space oxygen, ensuring that sauces, liquid breakfast cereals, and purees remain stable without the need for excessive chemical preservatives. The convenient spout design provides easy dispensing and resealability, appealing directly to modern consumer convenience trends.
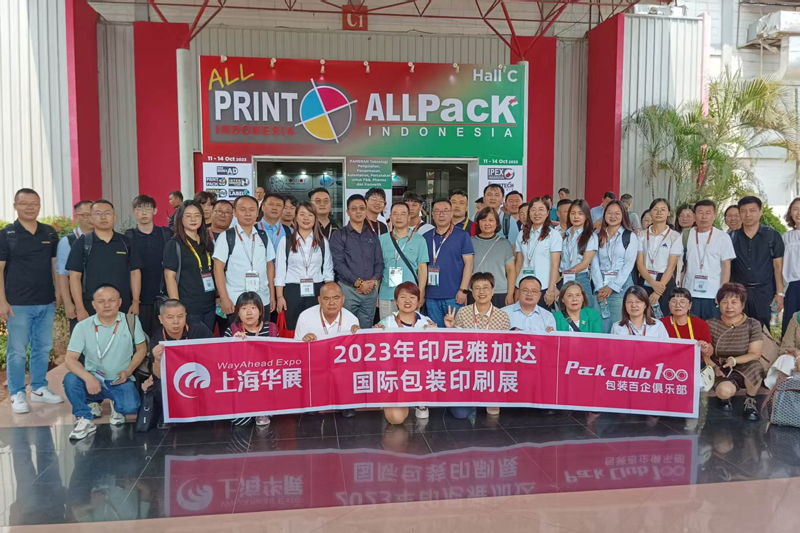
Connecting with partners globally and displaying our innovative packaging technologies at major international trade shows.
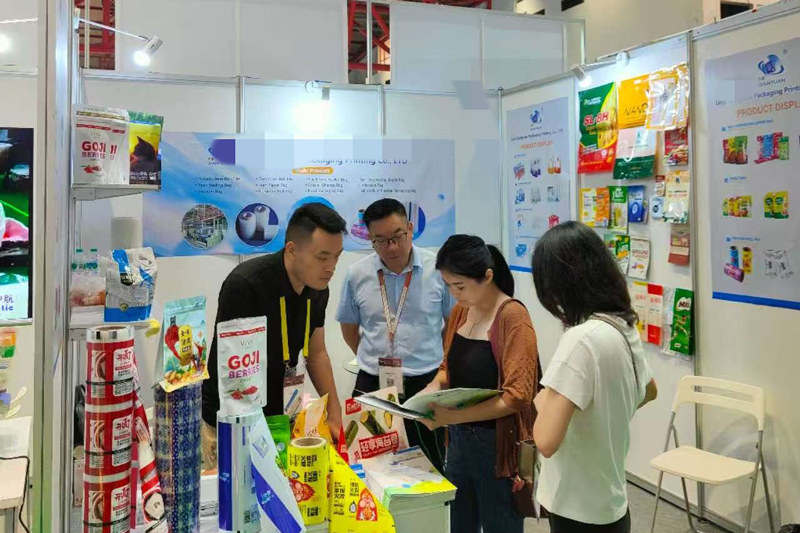
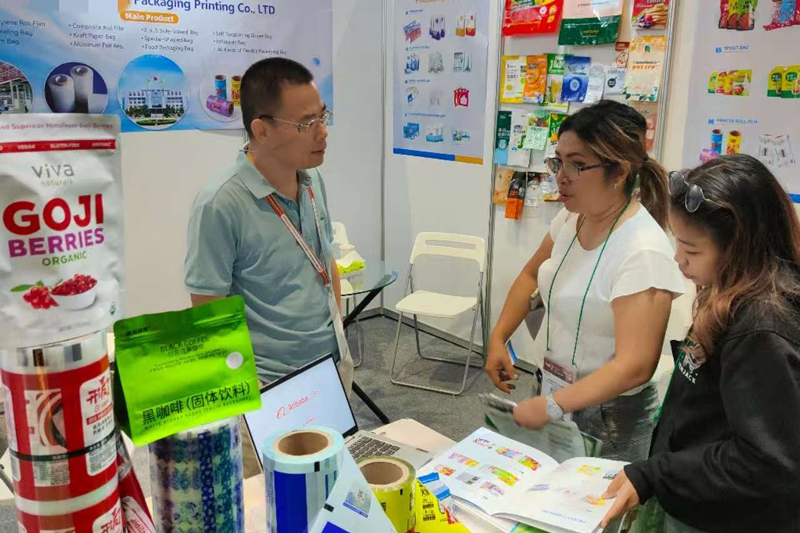
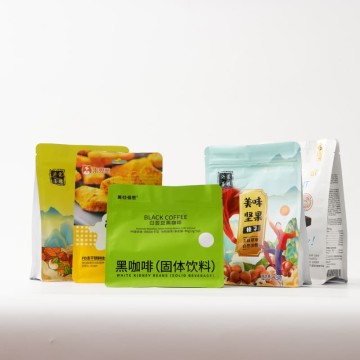
Select from our diverse product catalog tailored for commercial food processors, distributors, and brands.
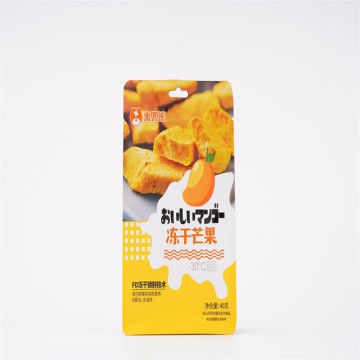
Since its establishment 23 years ago, relying on excellent product quality, comprehensive compliance guarantees, and efficient cross-border services, Jike Packaging Printing has established long-term cooperative relationships with customers in more than 50 countries and regions worldwide, serving clients including globally renowned food manufacturers, brand owners, and trading companies. In the future, we will continue to focus on changes in international market demand, using innovative technology and high-quality services as a link to become a trusted cross-border flexible packaging printing partner for global customers.
Contact Us