Welcome to our company
Leave Your Message
Explore our flagship resealable pouch formats engineered for optimal dispensing precision, extended shelf life, and superior burst resistance.
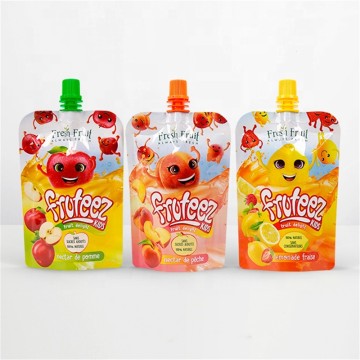
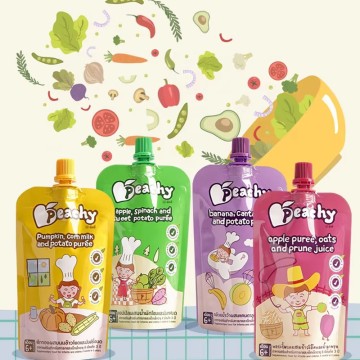
How flexible resealable plastic bags are replacing rigid bottles, metal cans, and glass jars across the global packaging landscape.
Multi-layered co-extrusion technology combining PET, Aluminum Foil, Oriented Polyamide (NY/OPA), and modified EVOH-PE to prevent oxygen permeation, maintain aroma, and prevent moisture loss for sensitive liquids.
Precision-engineered polyolefin fitments welded ultrasonically with high-pressure hermetic seals. Incorporating tamper-evident break rings, anti-choke safety caps, and child-resistant reclosable closures.
Over 75% reduction in raw material weight compared to traditional rigid containers, dramatically lowering freight transport emissions, warehouse space requirements, and full life-cycle carbon emissions.
The global packaging sector is witnessing a fundamental migration from rigid plastic bottles and glass jars toward flexible, resealable plastic pouches for liquid and paste formulations. Driven by increasing demand for on-the-go convenience, circular economy mandates, and logistical cost optimization, resealable plastic bags for convenient liquid pouching represent one of the fastest-growing segments in industrial flexible converting.
Unlike conventional single-use drink boxes or glass containers, modern spout pouches (frequently configured as stand-up Doypacks, corner-spouted pouches, or quad-seal liquid bags) offer superior functionality. The integration of high-flow diameter spouts, anti-burst corner seals, and high-tensile multi-layer substrates allows fluid manufacturers to package items ranging from low-viscosity beverages and cold brews to high-viscosity pastes, condiments, agrochemicals, and liquid detergents.
Engineered to withstand rigorous hot-fill, cold-chain, retort sterilization, and high-pressure logistical distribution.
From organic fruit purees, baby food, and smoothie blends to cold-brew coffees, energy drink concentrates, and craft alcoholic beverages. Complies with FDA and EU food contact safety regulations.
Ideal for mayonnaise, salad dressings, ketchup, cooking oils, and artisanal syrups. Eliminates food waste by enabling over 98% evacuation rate of thick viscous products through controlled squeeze dispensing.
Eco-friendly refill pouches for concentrated laundry detergents, surface disinfectants, liquid hand soaps, motor lubricants, and liquid fertilizers, drastically cutting household plastic consumption.
Liquid packaging imposes stringent mechanical demands on flexible plastic films. While dry product packaging primarily focuses on moisture barriers, liquid pouching must address internal hydraulic shock, hydrostatic head pressure, micro-leakage risks around the spout weld, and seal channel fatigue during transportation. Our resealable liquid pouches undergo rigorous quality testing, including:
Shandong Jike International Trade Co., Ltd. is a state-owned professional food packaging and printing enterprise, established in 2003 and located in Shandong Province, eastern China. The company has obtained and passed ISO9001, ISO14001, and ISO45001 certifications, and all our products have passed QS food safety certification.
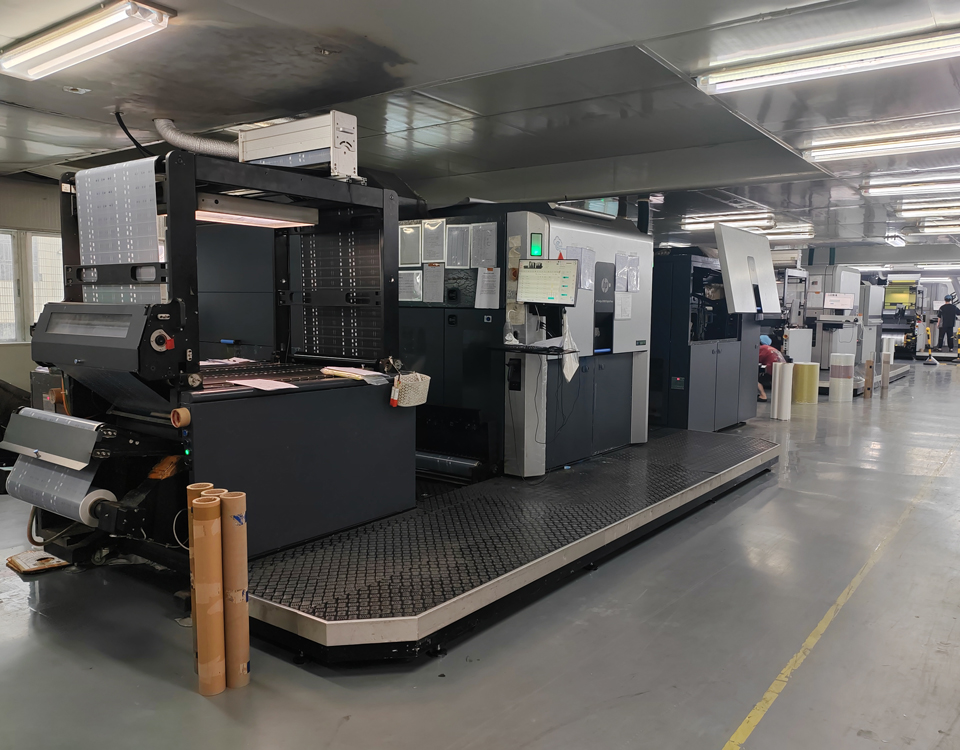
With over two decades of dedicated manufacturing, we have deployed modern high-speed 10-color rotogravure printing presses, solventless laminators, and automated spout-inserting pouch makers to supply high-end packaging solutions across North America, Europe, Southeast Asia, and the Middle East.
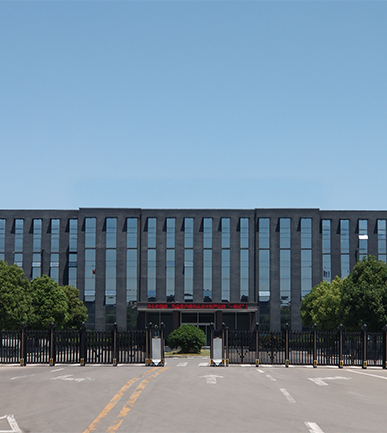
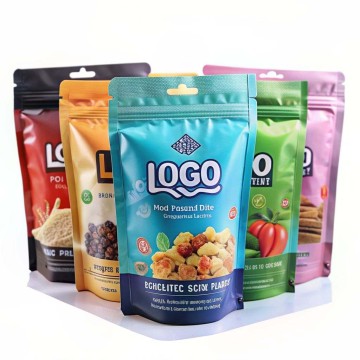
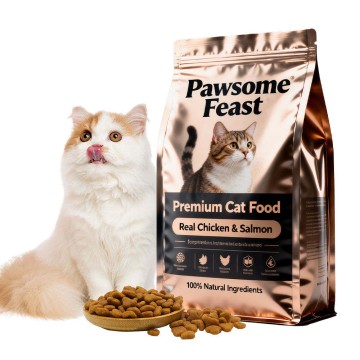
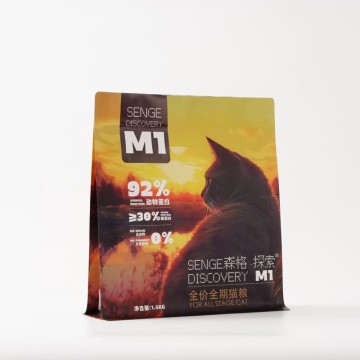
The company's core export products cover the needs of multiple industries, mainly including food-grade flexible packaging, pet food packaging, polyethylene film, and woven packaging bags, which can accurately match the market standards of different regions such as North America, the European Union, Southeast Asia, and the Middle East. We also support multi-language design and printing, barcode/QR code customization, material combination selection, and thickness selection to fully meet the needs of cross-border trade.
In terms of supply chain and service, the company has strong cross-border delivery capabilities. We have standardized production workshops and automated production lines, with flexible minimum order quantities for regular products. We undertake both small-batch customization and large-volume order production; we have established a strict quality control system, tracing the entire process from raw material procurement and production processing to finished product inspection, ensuring that every batch of products meets the quality standards of the importing country; and we are equipped with a professional cross-border logistics team to support various transportation methods such as full container shipping, LCL shipping, and air freight.
Connecting with leading worldwide brands, food processors, and supply chain partners at premier international trade events.
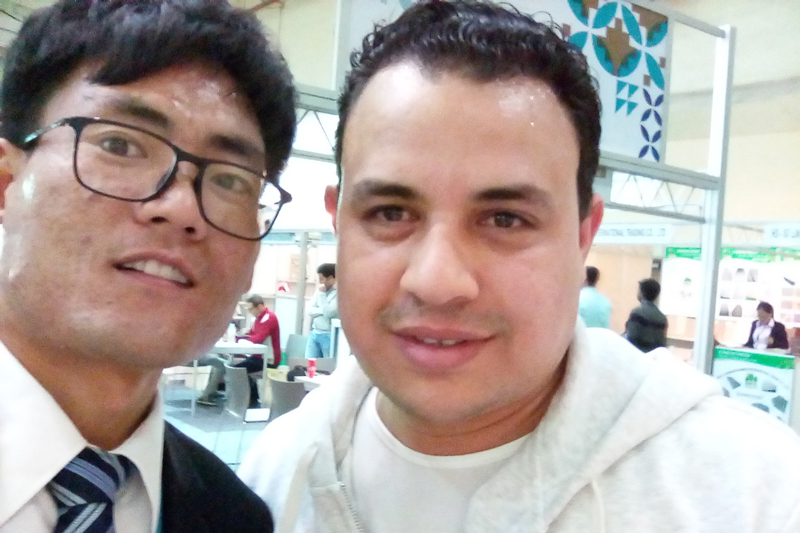
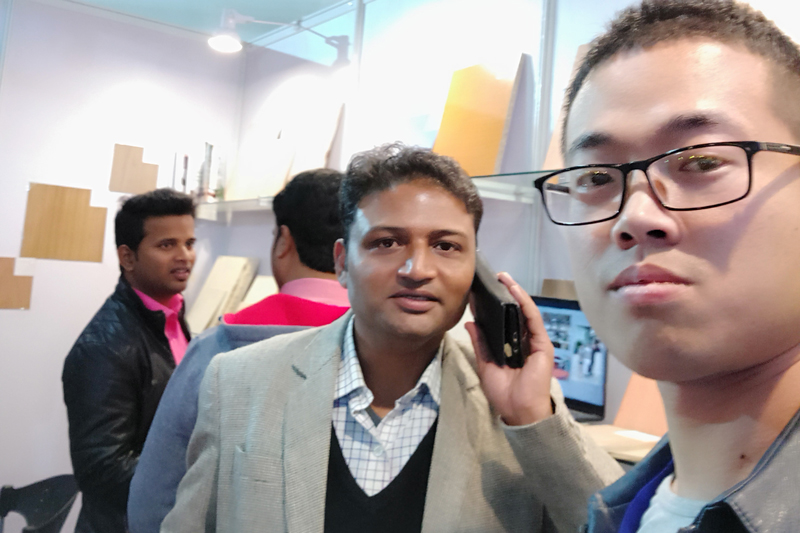
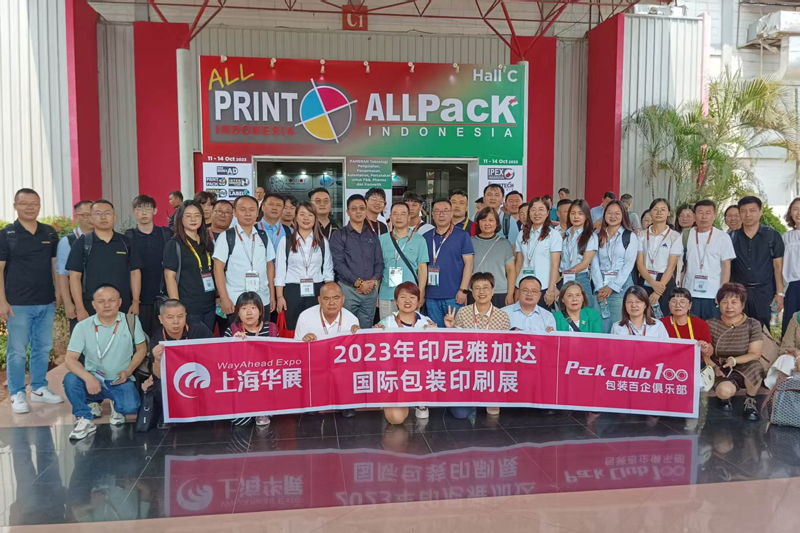
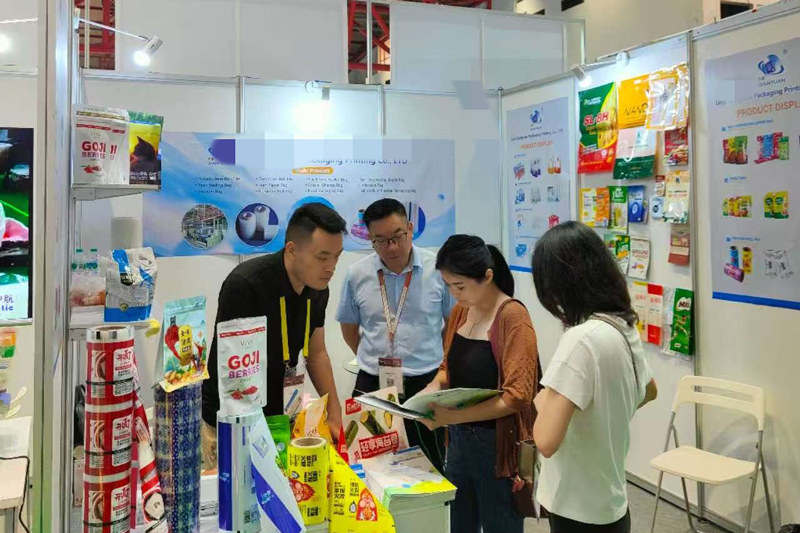
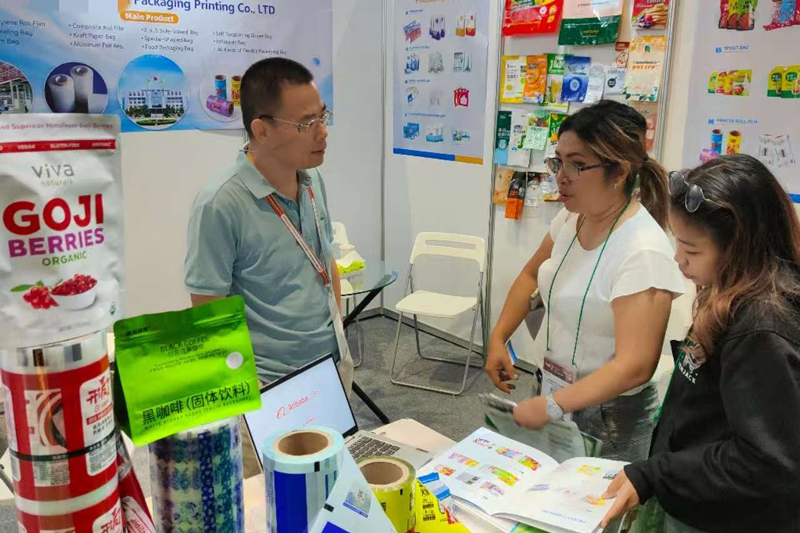
Since its establishment 23 years ago, relying on excellent product quality, comprehensive compliance guarantees, and efficient cross-border services, Jike Packaging Printing has established long-term cooperative relationships with customers in more than 50 countries and regions worldwide, serving clients including globally renowned food manufacturers, brand owners, and trading companies. In the future, we will continue to focus on changes in international market demand, using innovative technology and high-quality services as a link to become a trusted cross-border flexible packaging printing partner for global customers.
Contact Us TodayDiscover our comprehensive collection of custom printed stand-up bags, spout pouches, pet food packaging, and specialized barrier films.