Welcome to our company
Leave Your Message
Engineered with recyclable mono-materials and advanced barrier laminations for optimum product freshness, brand elevation, and minimal ecological footprint.
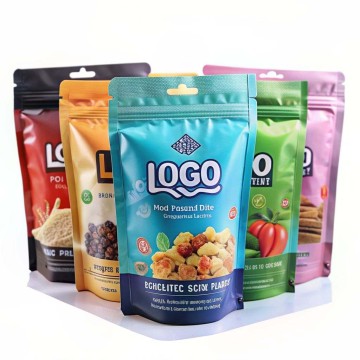
The global packaging sector is undergoing a profound structural transformation. Modern food manufacturers face a dual challenge: safeguarding product shelf-life and nutrient density while drastically curtailing virgin plastic utilization and carbon emissions. Historically, food packaging relied on multi-material multi-layer laminates—such as PET/Aluminum Foil/PE structures—which provided outstanding barrier protection against oxygen and moisture but proved virtually impossible to recycle in standard municipal recycling streams.
Today, with regulatory frameworks tightening worldwide (such as the European Packaging and Packaging Waste Regulation / PPWR, Extended Producer Responsibility / EPR mandates, and global plastic taxes), food brand owners are aggressively adopting printed food pouches engineered for eco-friendly recyclable packaging solutions. This circular shift is driven by breakthrough material science, including Machine-Direction Oriented Polyethylene (MDO-PE) and fully recyclable Mono-Polypropylene (Mono-PP) matrices equipped with high-barrier vacuum plasma coatings.
Engineered entirely from unified polymer streams (all-PE or all-PP) enabling straightforward mechanical sorting, washing, and reprocessing without composite delamination issues.
Replacing heavy aluminum foil with ultra-thin atomic barrier layers, delivering Water Vapor Transmission Rates (WVTR) and Oxygen Transmission Rates (OTR) below 0.5 cc/m²/day.
Employing low-VOC and non-toxic water-based inks capable of 9-color gravure and HD flexographic printing, maintaining vivid color gamuts with minimal environmental toxicity.
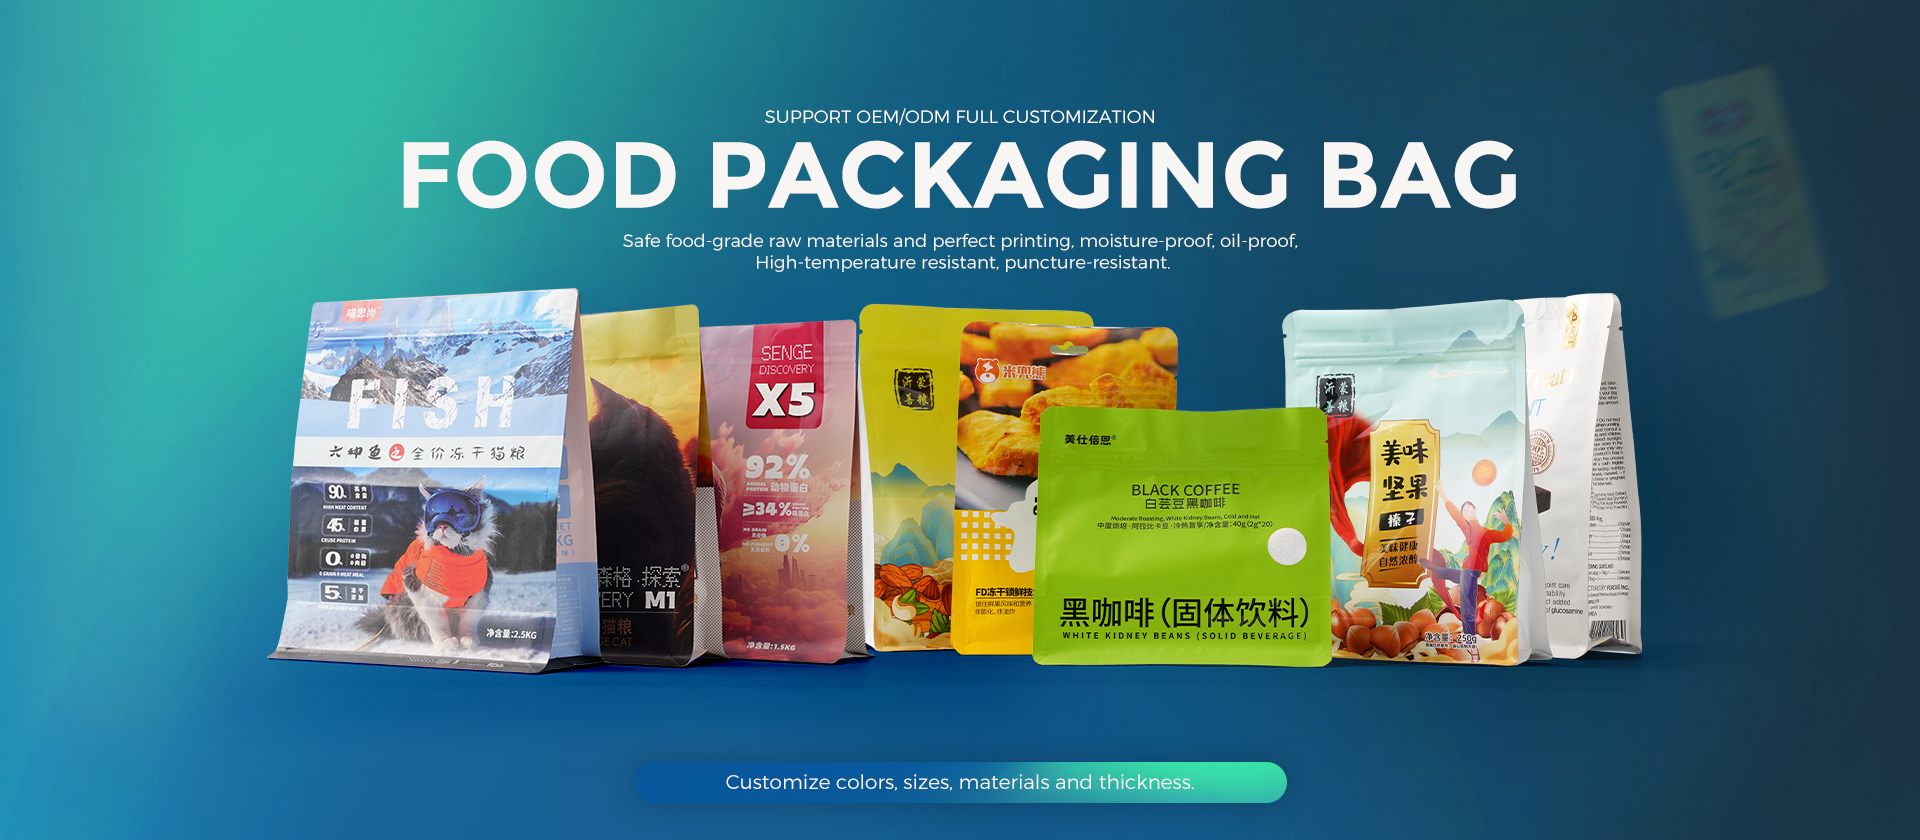
From sensitive whole bean coffee to high-temperature retort wet food, our customizable flexible structures deliver uncompromised mechanical strength and preservation performance.
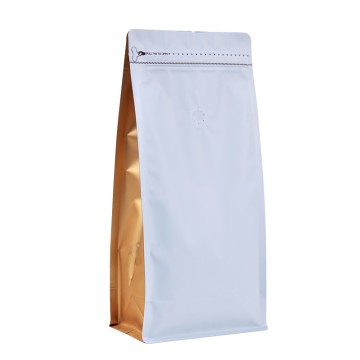
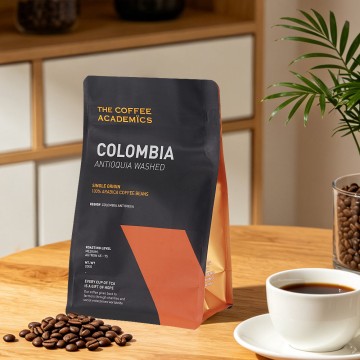
Integrated with mono-material PE degassing valves and 8-side flat bottom seals, these pouches shield volatile aromatic compounds from oxidation while venting internal CO2 buildup efficiently without compromising external barrier integrity.
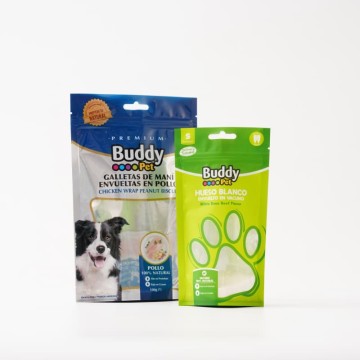
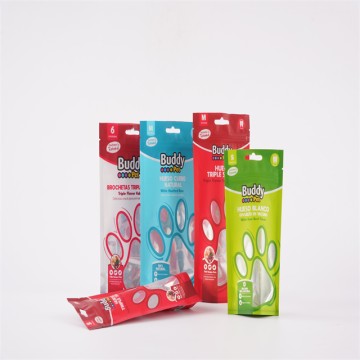
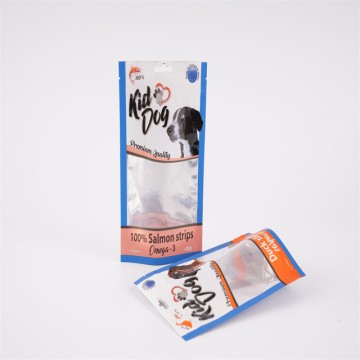
Tailored for high-protein pet treats, kibble, and wet cat food in jelly. Incorporates retortable grade films capable of withstanding 121°C to 135°C thermal sterilization processes, puncture-resistant sidewalls, and easy-open laser scoring.
Designed with high-tensile metallized film coatings to prevent lipid rancidity and moisture ingress. Features resealable press-to-close zippers, matte/gloss tactile finishes, and transparent display windows to showcase product quality.
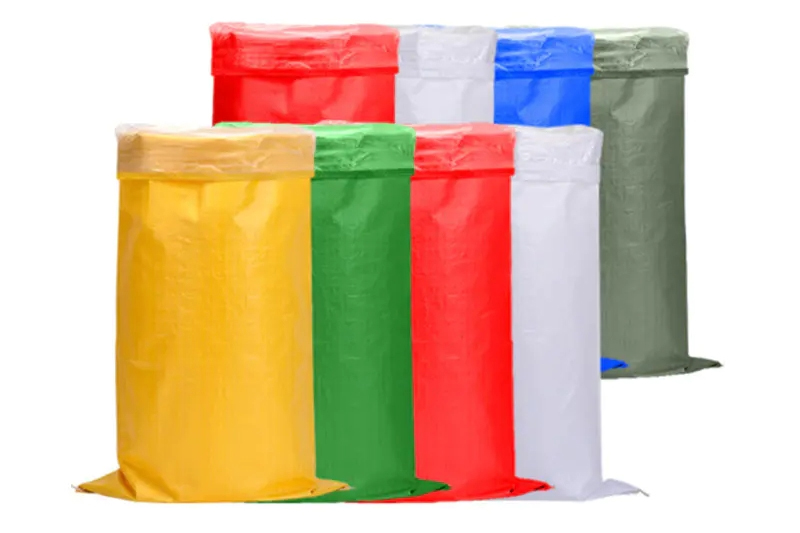
Laminated woven polypropylene (PP) sacks engineered for 5kg to 50kg bulk packaging. Offers superior tear strength, drop resistance, micro-perforated aeration, and high-impact flexographic branding for industrial and retail distribution.
Shandong Jike International Trade Co., Ltd. is a premier state-owned professional food packaging and printing enterprise, founded in 2003 and centrally located in Shandong Province, eastern China. Over the past 22+ years, Jike has developed an integrated, end-to-end industrial value chain spanning flexible food packaging bags, high-barrier pet food pouches, and heavy-duty laminated PP woven sacks.
Our facilities boast an annual production capacity exceeding 5,000 tons of flexible food pouches and 3,000 tons of high-strength woven packaging. Operating under stringent international quality control protocols, we hold full ISO9001 Quality Management, ISO14001 Environmental Management, and ISO45001 Occupational Health and Safety certifications, alongside full QS food safety compliance. We provide multi-language prepress color separation, QR/barcode traceability coding, and customized resin formulations tailored to cross-border food trade compliance.

Comprehensive portfolio covering food packaging pouches, pet food bags, and agricultural woven sacks all under one roof.

End-to-end customization from pouch geometry, zipper styles, gusset profiles to material barrier thickness and surface finishes.

Multi-stage testing covering raw resin purity, chromatic ink density, lamination peel strength, seal hermeticity, and drop tests.

Reliable freight management offering LCL, FCL container loads, and expedited courier delivery (DHL/FedEx) direct to your warehouse.
Stay informed on circular economy mandates, advanced polymer developments, and high-efficiency packaging strategies.
As global demand for sustainable packaging accelerates, mono-polypropylene configurations deliver robust tensile resilience and clean recycling streams...
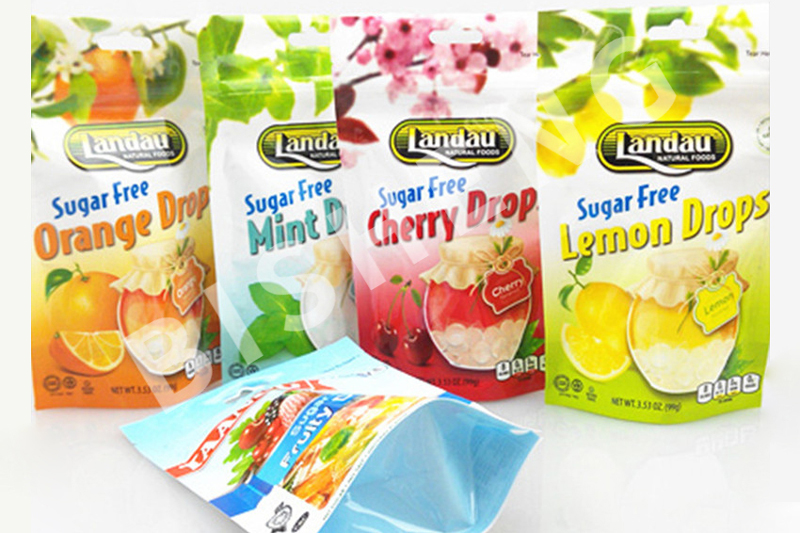
Stand-up pouches deliver unmatched on-shelf visibility, reduction in logistics tare weight, and superior hermetic reclosability compared to rigid containers...
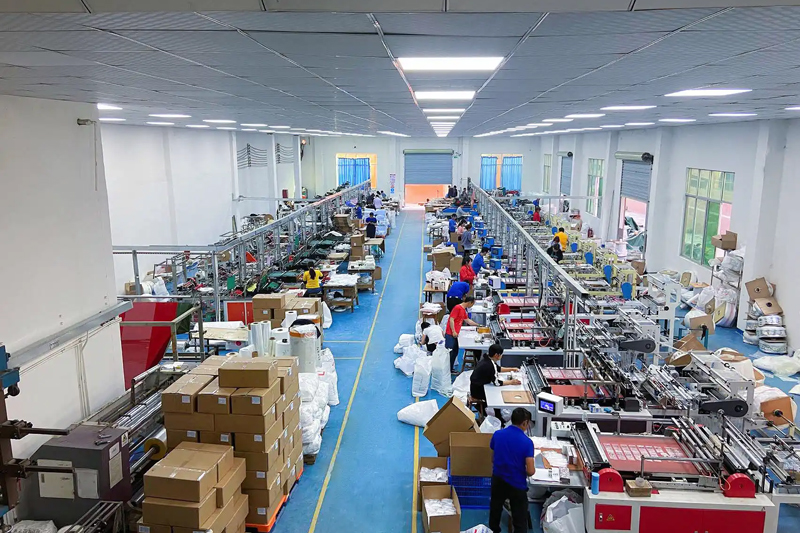
Anticipating structural regulatory milestones, smart QR interactive packaging integration, and next-generation barrier coatings in the global food sector...
Looking to transition your food brand to recyclable mono-material pouches or develop a custom barrier specification? Connect directly with our engineering and packaging design team.
Precision engineered for dry bulk, liquids, confectionery, premium coffee, and pet snacks with custom printing and high-barrier properties.