Welcome to our company
Leave Your Message
Precision-engineered PP woven bags and flexible pouches for liquid, food, and specialty packaging needs — fully customizable for global markets.
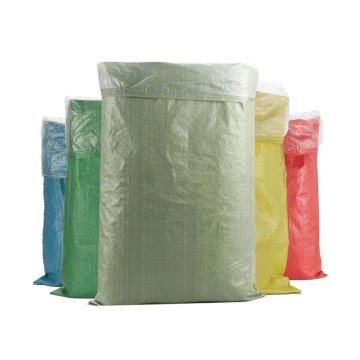
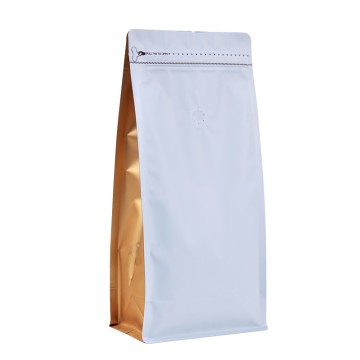
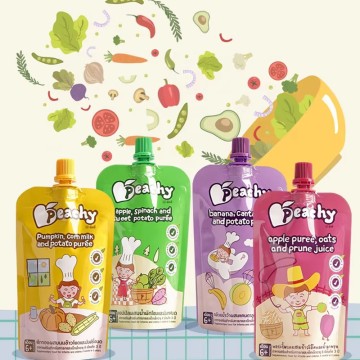
In today's rapidly evolving global packaging industry, PP woven bags for convenient resealable liquid pouching have emerged as one of the most versatile, cost-effective, and environmentally responsible solutions across a wide spectrum of commercial and industrial applications. Polypropylene (PP) woven fabric — constructed from interlaced strips of oriented polypropylene — delivers an exceptional combination of tensile strength, moisture resistance, and structural integrity that traditional paper or single-layer plastic packaging simply cannot match.
The global flexible packaging market, valued at over USD 250 billion in 2023, continues to expand at a compound annual growth rate (CAGR) exceeding 4.5% through 2030. Within this landscape, resealable liquid pouching solutions built on PP woven substrates are capturing significant market share, driven by surging demand from the food & beverage, agriculture, chemical, and e-commerce logistics sectors. Brands and manufacturers worldwide are actively transitioning from rigid containers and conventional plastic bags to laminated PP woven pouches with integrated zipper or spout closures — a shift that reduces material consumption by up to 40% while enhancing shelf appeal and consumer convenience.
The resealable PP woven liquid pouch market is projected to grow at 6.2% CAGR through 2030, driven by e-commerce growth, food safety regulations, and the global push toward sustainable, lightweight packaging alternatives.
The adoption of PP woven bags for liquid pouching is no longer confined to a single industry. Today, this packaging format serves as a critical infrastructure component across multiple commercial and industrial verticals:
Food & Beverage Manufacturing: From juice concentrates and sauces to edible oils and dairy products, food processors rely on laminated PP woven pouches with resealable spouts or zipper closures to preserve product freshness, extend shelf life, and meet food-grade safety standards including FDA, EU 10/2011, and China GB regulations. The ability to print high-resolution branding directly on the woven surface further enhances retail shelf presence.
Agricultural & Horticultural Sector: Liquid fertilizers, pesticide concentrates, and irrigation additives require robust packaging that withstands chemical exposure, UV radiation, and rough handling during distribution. PP woven bags laminated with BOPP or PE inner liners provide the chemical resistance and puncture strength required for safe transport of these sensitive liquids, while resealable closures allow farmers to use partial quantities without product degradation.
Chemical & Industrial Fluids: Industrial lubricants, adhesives, cleaning agents, and specialty chemicals are increasingly being packaged in bulk PP woven intermediate bulk containers (IBCs) and resealable pouches. These formats reduce packaging waste, lower shipping costs due to lighter tare weight, and comply with international hazardous materials transport regulations when properly constructed.
E-Commerce & Direct-to-Consumer Brands: The explosive growth of online retail has created massive demand for packaging that is both leak-proof and resealable for liquid products such as shampoo, detergent refills, cooking oils, and health supplements. PP woven resealable pouches offer the structural rigidity needed to survive warehouse handling and last-mile delivery without leakage or deformation.
Manufacturers are increasingly adopting mono-material PP constructions that maintain full recyclability without sacrificing barrier performance. Bio-based PP derived from sugarcane and post-consumer recycled (PCR) PP content are gaining traction as brands respond to ESG commitments and extended producer responsibility (EPR) legislation across the EU and North America.
QR codes, NFC tags, and freshness indicators are being embedded into PP woven pouch designs, enabling brands to deliver product traceability, anti-counterfeiting protection, and interactive consumer engagement. This digital layer transforms the pouch from a passive container into an active communication channel — a critical differentiator in premium food and pharmaceutical markets.
Advanced circular loom technology combined with AI-driven quality inspection systems now enables PP woven bag manufacturers to achieve production speeds exceeding 200 meters per minute with defect detection accuracy above 99.5%. This automation dramatically reduces per-unit costs, making resealable liquid pouching solutions accessible to small and medium enterprises globally.
As global trade regulations tighten, leading PP woven bag suppliers now offer pre-certified packaging solutions compliant with FDA (USA), EU food contact materials regulations, REACH, RoHS, and regional standards across Southeast Asia and the Middle East — reducing time-to-market for brand owners entering new geographies.
Next-generation zipper profiles, child-resistant closures, and tamper-evident spout systems are being integrated directly into PP woven bag constructions. These innovations address regulatory requirements for hazardous liquid packaging while improving consumer convenience — a dual benefit that is accelerating adoption in both retail and industrial markets.
The transition from rigid drums and jerricans to flexible PP woven bulk liquid bags (FIBCs) is reshaping industrial logistics. A 1,000-liter PP woven bulk liquid container weighs as little as 3–5 kg versus 15–20 kg for equivalent rigid containers, delivering significant freight cost savings and reducing carbon emissions across global supply chains.
From food production lines to industrial distribution networks, PP woven resealable liquid pouches are transforming how liquids are stored, transported, and consumed across industries.
Laminated PP woven spout pouches maintain the flavor integrity of juice concentrates and functional beverages during extended storage. The resealable spout enables portion control for foodservice operators, reducing waste and improving operational efficiency in commercial kitchens and catering environments.
High-strength PP woven pouches with chemical-resistant LDPE inner liners are the preferred format for packaging liquid NPK fertilizers, humic acid solutions, and crop protection chemicals. Resealable closures prevent accidental spills during field application, while UV-stabilized outer fabrics protect product integrity during outdoor storage.
Shampoo, conditioner, liquid soap, and household cleaning product refills in resealable PP woven pouches are gaining popularity as eco-conscious consumers seek to reduce single-use plastic consumption. Brands benefit from 60–70% less plastic versus rigid bottles while delivering the same premium product experience.
The booming USD 150+ billion global pet care market is driving rapid adoption of resealable liquid pouches for wet pet food, bone broth, and veterinary supplements. PP woven constructions provide the puncture resistance needed to protect against claw damage during storage, while zipper closures maintain freshness between servings.
Automotive and industrial maintenance sectors are transitioning to bulk PP woven flexible containers for lubricating oils, hydraulic fluids, and specialty greases. These containers reduce packaging material costs by up to 50% compared to rigid drums while enabling precise dispensing through integrated spout systems.
Cold brew coffee concentrates, premium sauces, artisan condiments, and specialty food liquids are leveraging high-barrier PP woven laminate pouches with one-way degassing valves and resealable zippers to deliver café-quality products to retail consumers with extended shelf life and minimal preservative requirements.
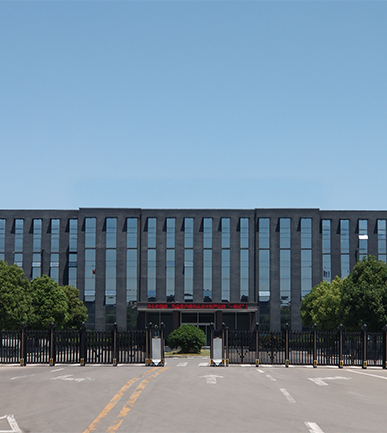
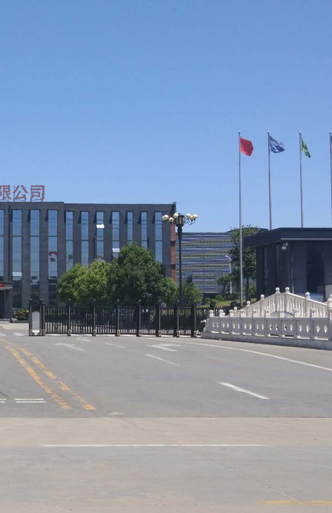
Shandong Jike International Trade Co., Ltd. is a state-owned professional food packaging and printing enterprise, established in 2003 and located in Shandong Province, eastern China. The company has obtained and passed ISO9001, ISO14001, and ISO45001 certifications, and all our products have passed QS food safety certification.
With over 23 years of production experience, we have built a reputation for delivering precision-engineered PP woven bags, resealable liquid pouches, and flexible packaging solutions that meet the exacting standards of global buyers across food, agriculture, chemical, and industrial sectors.
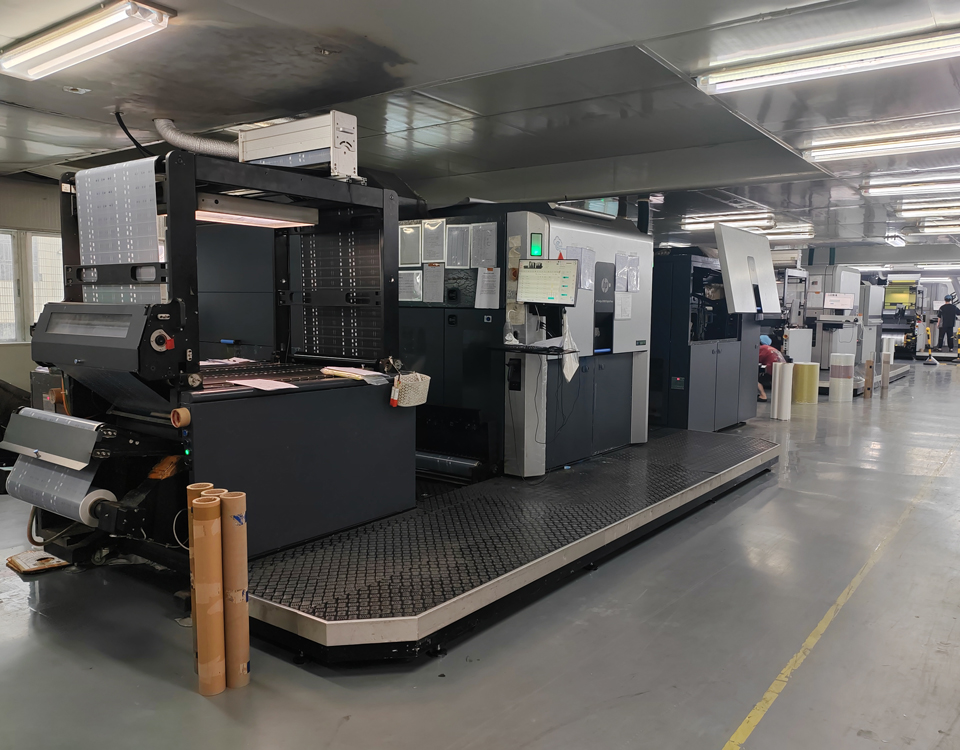
The company's core export products cover the needs of multiple industries, mainly including food-grade flexible packaging, pet food packaging, polyethylene film, and woven packaging bags, which can accurately match the market standards of different regions such as North America, the European Union, Southeast Asia, and the Middle East.
We also support multi-language design and printing, barcode/QR code customization, material combination selection, and thickness selection to fully meet the needs of cross-border trade. Our PP woven resealable liquid pouches are engineered to deliver superior performance in demanding environments — from refrigerated food distribution to outdoor agricultural storage.
Every product leaving our facility undergoes rigorous multi-stage quality inspection, ensuring that seam integrity, barrier performance, and print quality consistently exceed international buyer expectations.
In terms of supply chain and service, the company has strong cross-border delivery capabilities. We have standardized production workshops and automated production lines, with flexible minimum order quantities for regular products. We undertake both small-batch customization and large-volume order production.
We have established a strict quality control system, tracing the entire process from raw material procurement and production processing to finished product inspection, ensuring that every batch of products meets the quality standards of the importing country. We are equipped with a professional cross-border logistics team to support various transportation methods such as full container shipping, LCL shipping, and air freight.
Our global logistics network ensures that your PP woven resealable liquid pouching orders arrive on schedule, in perfect condition, with full documentation compliance for customs clearance in any destination market.
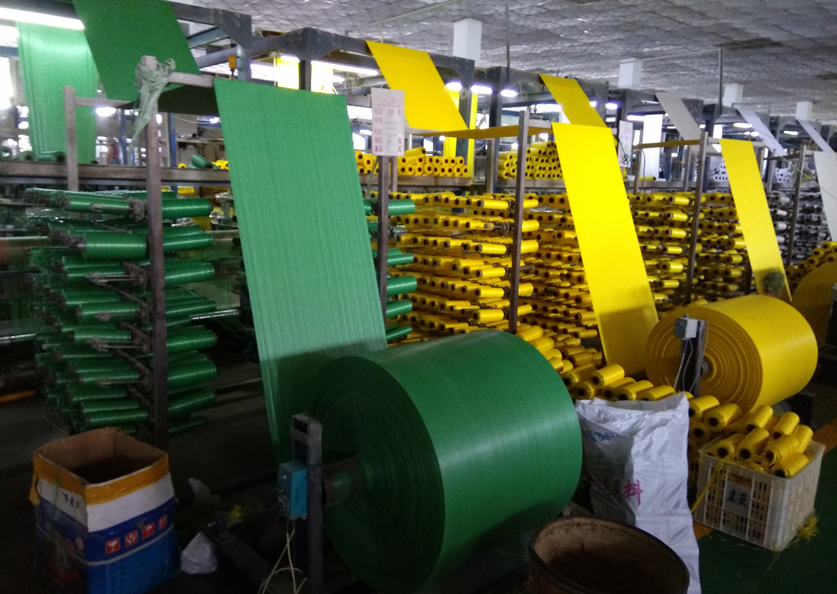
The technical architecture of a high-performance PP woven resealable liquid pouch involves multiple layers of material science expertise. The base fabric — woven from oriented polypropylene tapes at a density of 8–14 tapes per inch — provides the structural backbone. Lamination with BOPP (biaxially oriented polypropylene), PE (polyethylene), or EVOH (ethylene vinyl alcohol) inner layers creates the barrier performance required to contain liquids without seepage or permeation.
At Jike Packaging, our R&D team continuously evaluates emerging polymer formulations to enhance the performance of our PP woven liquid pouching solutions. Current material innovations include:
The resealability function is central to the value proposition of modern PP woven liquid pouches. Our manufacturing capabilities encompass the full spectrum of closure technologies:
Every PP woven resealable liquid pouch produced at our facility undergoes 100% seal integrity testing, drop-test validation, and migration testing for food-contact applications — ensuring zero-defect delivery to our global customers.
Jike Packaging actively participates in leading global packaging and trade exhibitions, showcasing our latest PP woven resealable liquid pouching innovations to buyers from over 70 countries.
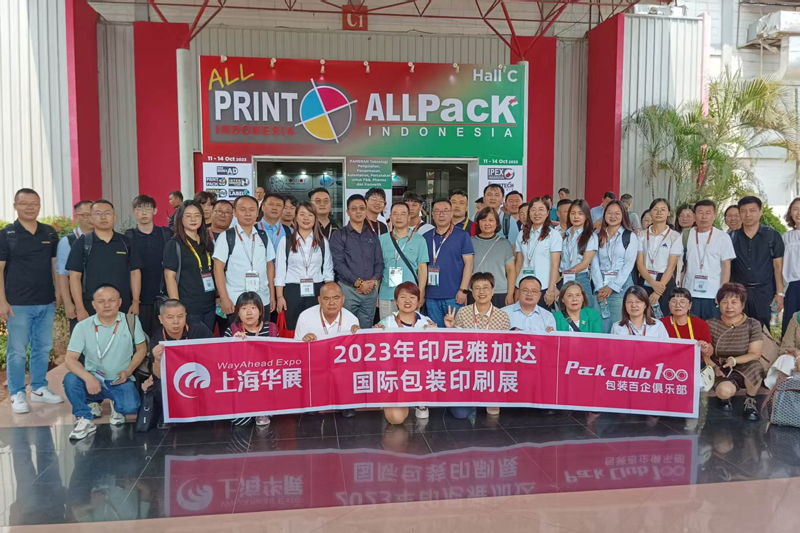
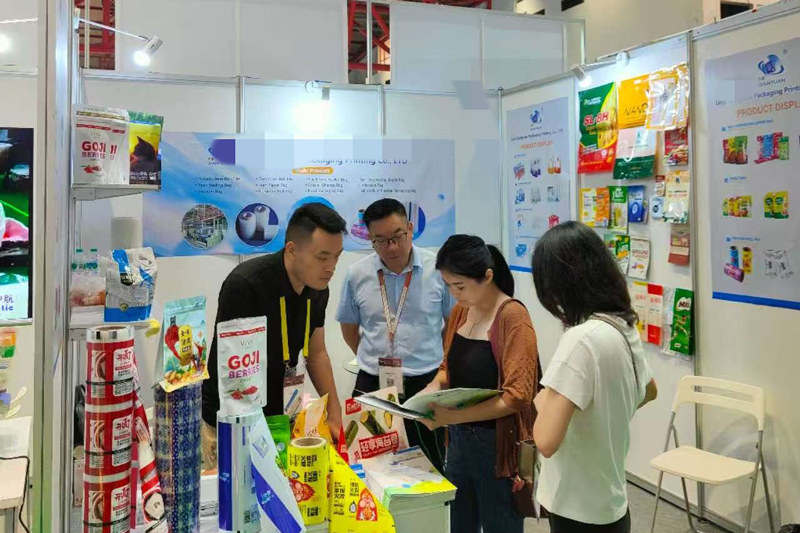
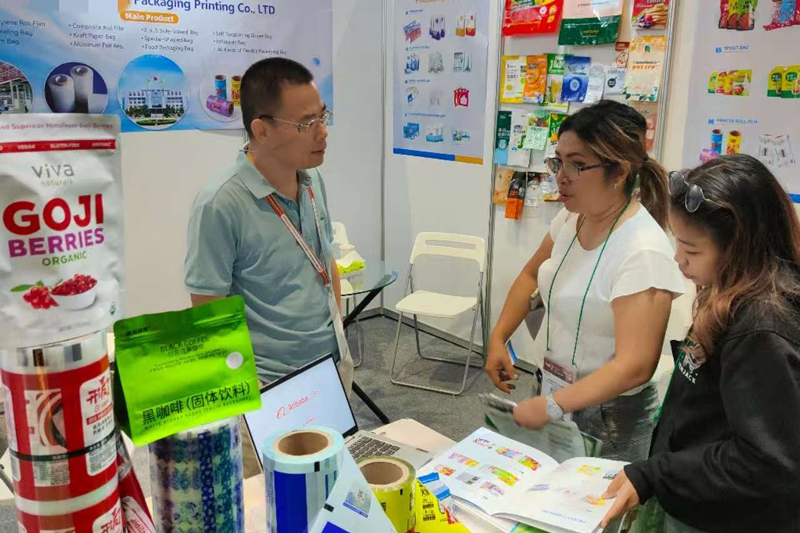
Since its establishment 23 years ago, relying on excellent product quality, comprehensive compliance guarantees, and efficient cross-border services, Jike Packaging Printing has established long-term cooperative relationships with customers in more than 50 countries and regions worldwide, serving clients including globally renowned food manufacturers, brand owners, and trading companies. In the future, we will continue to focus on changes in international market demand, using innovative technology and high-quality services as a link to become a trusted cross-border flexible packaging printing partner for global customers.
Contact Us