Welcome to our company
Leave Your Message
Next-Gen Barrier Technology • Smart Food Packaging

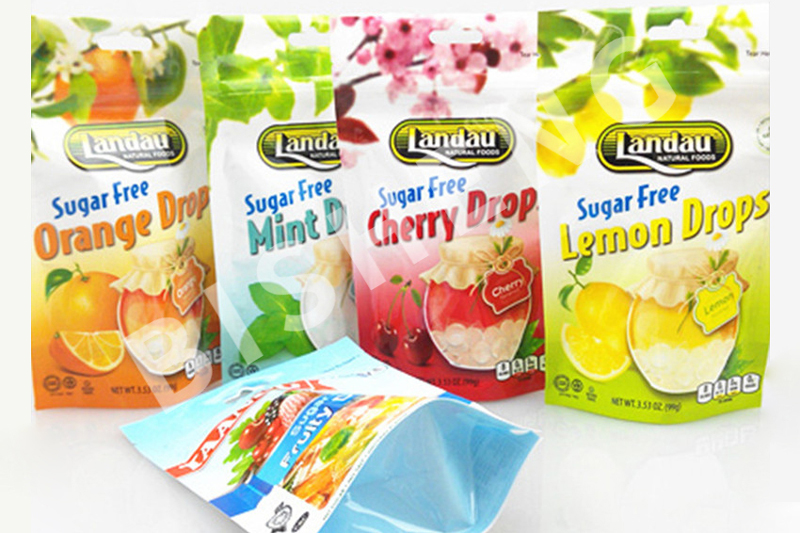
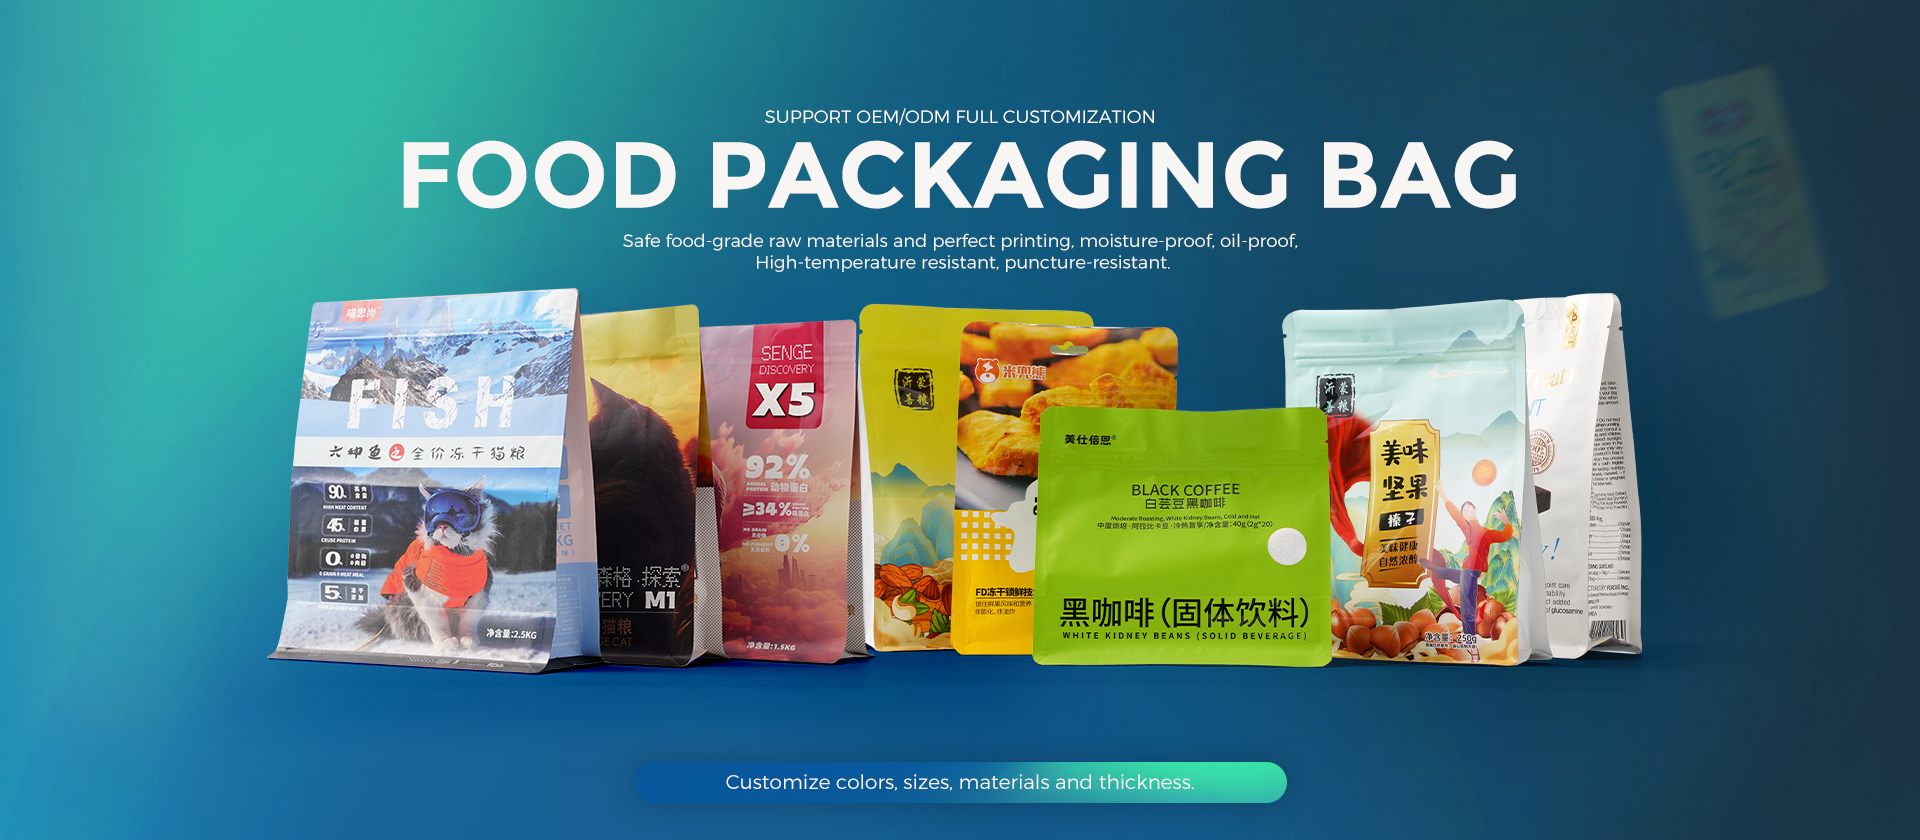
Food Grade Packaging Bag For Retail-Ready Printed Food Branding

Precision-engineered multi-layer food barrier pouches, high-speed rotogravure printed films, and shelf-optimized custom flexible packaging designed for maximum brand conversion and sustainable global shelf life.

Featured Retail-Ready Food Packaging Pouches

Engineered for high-impact retail shelves: barrier-protected, FDA/QS-certified, and custom printed to accelerate consumer brand awareness.

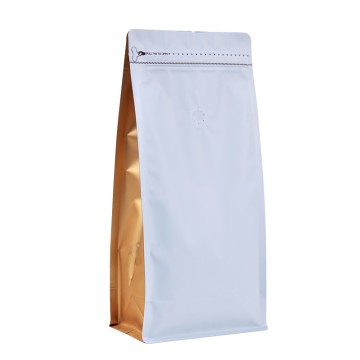
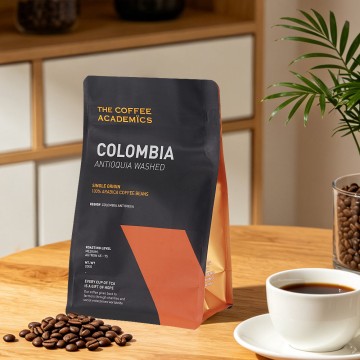
Retail-Ready Custom Printed Coffee Bags with Degassing Valve

High-barrier 8-side seal matte pouches featuring one-way degassing valves to lock in roasted aroma and prevent oxidative degradation.

View Product Specifications →

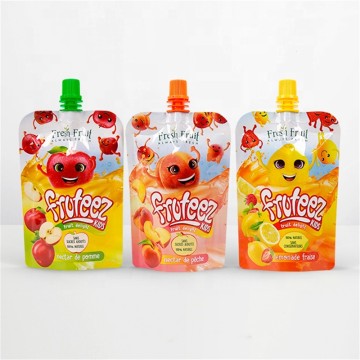
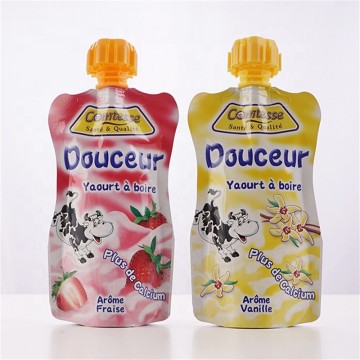
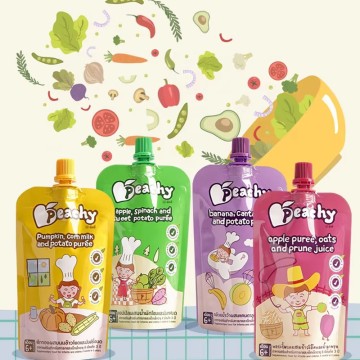
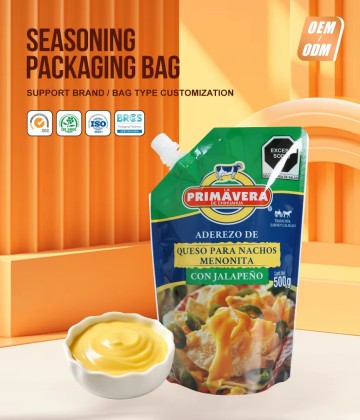
Ergonomic Liquid & Sauce Doypack Spout Pouches

Anti-burst flexible liquid doy-packs with tamper-evident spouts, tailored for cold-press juices, culinary purees, and ready beverages.

View Product Specifications →

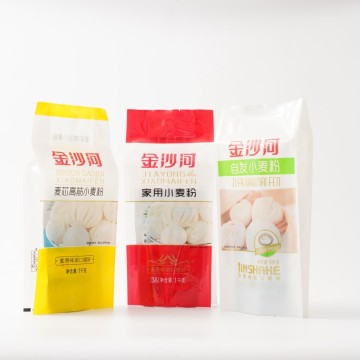
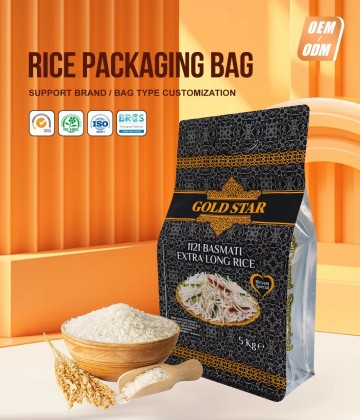
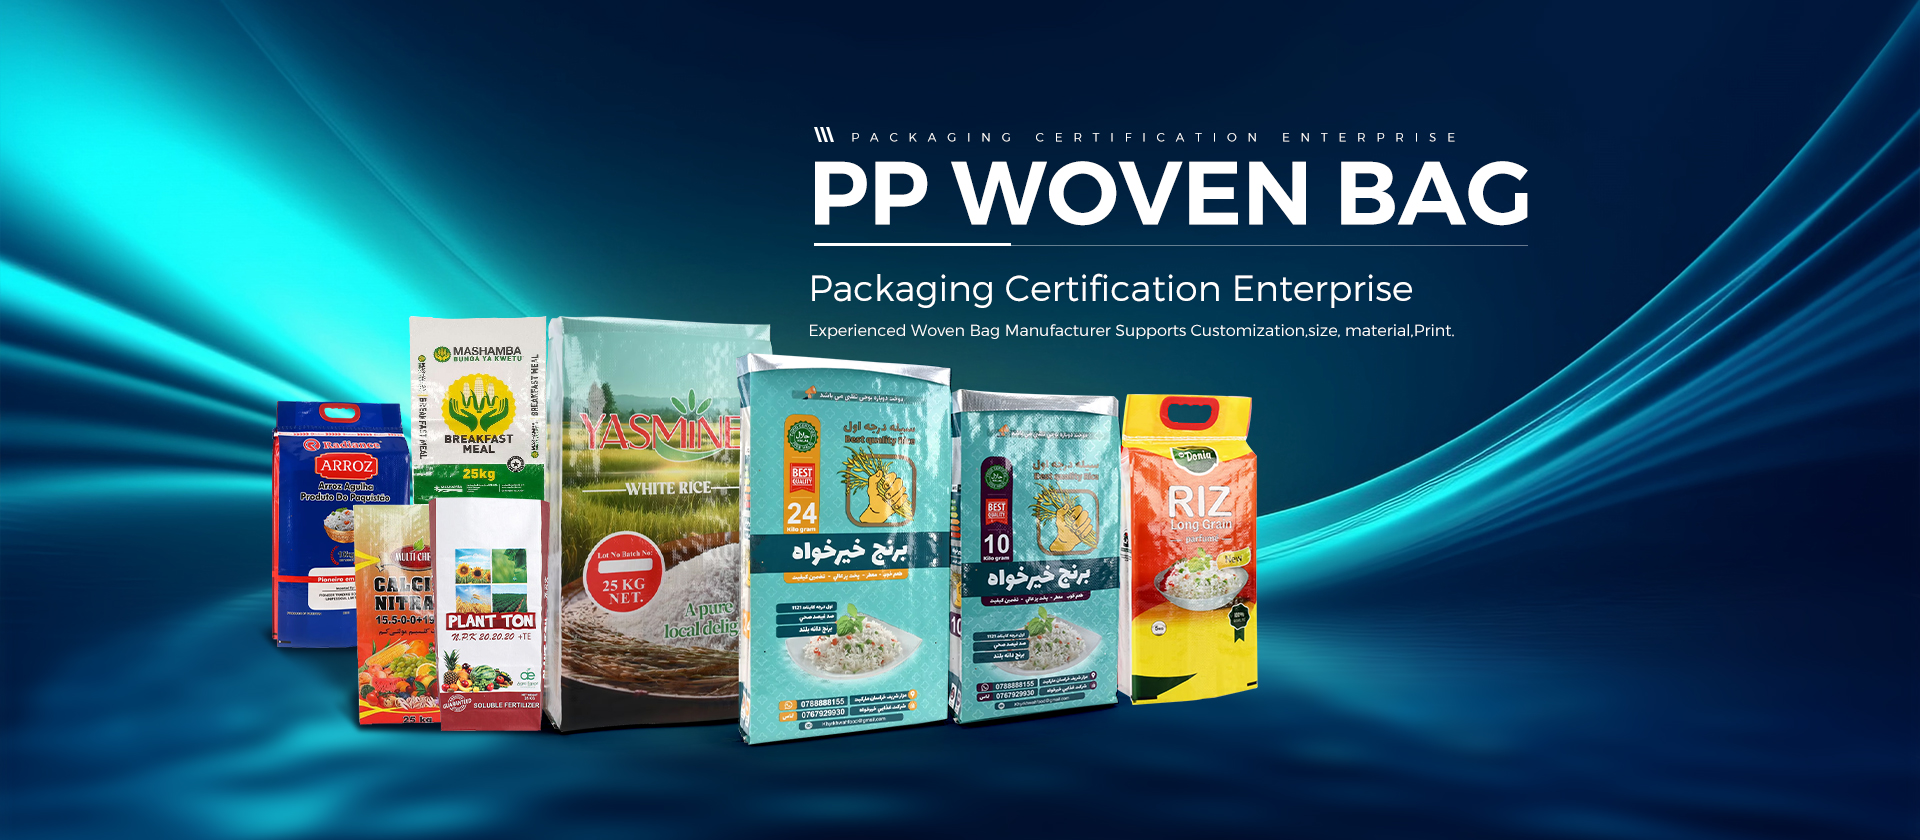
Premium High-Strength Grain & Rice Storage Pouches

Heavy-duty hermetic barrier laminated bags designed for bulk grains, pulses, and seeds with reinforced anti-drop handles.

View Product Specifications →

Scalable Reusable Food-Grade Liquid Barrier Pouch

Versatile 100ml-500ml stand-up volume configuration with airtight corner valve, preventing moisture ingress and bacterial cross-contamination.

View Product Specifications →

Commercial Dynamics: The Power of Retail-Ready Food Branding

Why modern food FMCG brands are transitioning from rigid packaging to intelligent, high-barrier flexible pouches.

Advanced Hermetic Shielding

Micro-layered co-extruded films including EVOH, AL Foil, and metallized PET shield active nutritional compounds from UV light, moisture vapor, and volatile organic compound degradation.

High-Def Retail Shelf Appeal

Utilizing 9-to-11 color rotogravure printing, spot-UV varnish, and soft-touch tactile finishes to maximize FMCG visual prominence on competitive hypermarket shelves.

Reduced Carbon Logistics

Flexible food pouches weigh up to 75% less than glass jars or rigid tin cans, slashing logistics emissions, warehousing volume, and retail footprint dramatically.

The Shift Toward Retail-Ready Packaging (RRP) in Modern FMCG

In the contemporary supermarket and e-commerce landscape, packaging is no longer merely a protective vessel; it acts as the primary frontline ambassador of the food brand. "Retail-Ready Packaging" (RRP) and "Shelf-Ready Packaging" (SRP) mandate that every food-grade packaging bag must fulfill dual mandates: operational efficiency from transport to shelf, and instantaneous visual conversion at the point of consumer purchase.

Global regulatory bodies, including the US FDA, European EFSA, and China's National Food Safety Standard (GB 4806), enforce rigorous migration limits on packaging films. A compliant food-grade packaging bag prevents plasticizer transfer, eliminates solvent residual toxins, and maintains organoleptic purity—ensuring that dry foods, liquids, and bio-sensitive organic snacks preserve their genuine flavors, aroma, and crispness without synthetic preservation additives.

Multi-Layer Material Architecture Explained

Achieving superior barrier properties while preserving vibrant, photo-realistic brand graphics requires multi-ply polymer laminations engineered specifically for each food matrix:

Material Combination Key Barrier Function Target Food Applications Retail Merchandising Benefit
PET / AL / PE Near-zero Oxygen & Water Vapor Transmission Rate (WVTR < 0.05g/m²/day) Specialty Roasted Coffee Beans, Infant Milk Formula, Dehydrated Organics Rigid standing profile; metallic foil finish preserves 18-24 months freshness.
BOPP / Kraft / PE Eco-natural tactile feel with internal moisture barrier Organic Granola, Artisanal Bakery, Dried Nuts & Superfood Powders Appeals to clean-label, health-conscious consumers; premium earth-tone aesthetics.
PET / NY / PE (Retortable) High puncture resistance, thermal tolerance up to 121°C, oil resistance Liquid Sauces, Soups, Ready-to-Eat (RTE) Curries, Wet Pet Treats Eliminates heavy tin cans; microwave-safe convenience and spill-proof spout dispensing.
MDO-PE / PE (Mono-material) 100% Recyclable circular economy compliance (RIC 4) Confectionery, Dry Pasta, Dried Fruit Snacks, Pet Kibble Meets European EPR (Extended Producer Responsibility) packaging taxation rules.

Industrial Application Scenarios & Future Trends

Exploring how brand identity combines with food science across diverse processing environments.

Specialty Roasteries & Beverage

Specialty Coffee & Degassing Dynamics

Freshly roasted whole-bean coffee releases massive volumes of carbon dioxide (up to 10 liters per kilogram). Our multi-layer coffee packaging integrates automated ultrasonic degassing valves that release CO₂ while preventing oxygen from triggering staling. Custom matte lacquer printing elevates third-wave artisan roasteries onto luxury retail shelves.

Modern Condiments & Purees

Aseptic Liquid Spout Doypack Solutions

Replacing traditional heavy glass and rigid HDPE jugs, our spout doy-packs provide tamper-evident caps and puncture-resistant nylon barriers. Ideal for fruit purées, salad dressings, and organic sauces, these bags deliver accurate pouring, prevent post-use oxidation, and drastically diminish shipping cube weight.

Dry Bulk & Grain Staple Foods

Hermetic Grain, Rice & Pulse Packaging

Bulk staples face insect infestation, humidity absorption, and seam failure during multi-leg international shipping. Our laminated woven and heavy-gauge co-extruded stand-up bags offer vacuum-retaining seals, micro-perforated one-way vent channels, and ergonomically reinforced die-cut carry handles.

Animal Nutrition & Wellness

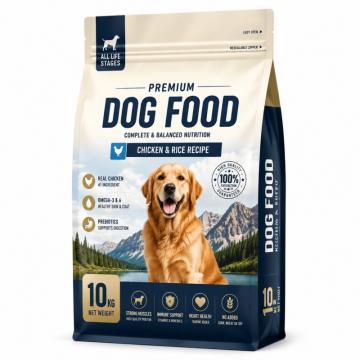
High-Capacity Pet Food & Treat Pouches

The humanization of pet nutrition demands human-grade food packaging. Our flat-bottom quad-seal bags feature odor-barrier inner liners, laser-scored easy-tear strips, and heavy-duty press-to-close zippers. Vibrant CMYK branding reassures pet owners of premium, nutrient-dense formulation inside.

Active & Smart Packaging

Intelligent Freshness & Traceability QR Codes

The convergence of AI traceability and packaging enables brand owners to print unique variable QR codes on each pouch. Consumers scan to verify batch safety, harvest origin, and farm-to-table supply chain certifications, fostering uncompromising consumer trust.

Circular Economy & ESG

Post-Consumer Recycled & Compostable Films

Aligning with 2026+ sustainability mandates, our mono-material polyethylene structures and certified industrial compostable PLA/PBAT films deliver robust barriers while fulfilling multinational brands' commitments to circular waste stream stewardship.

Rigorous Food-Grade Safety and Process Quality Control

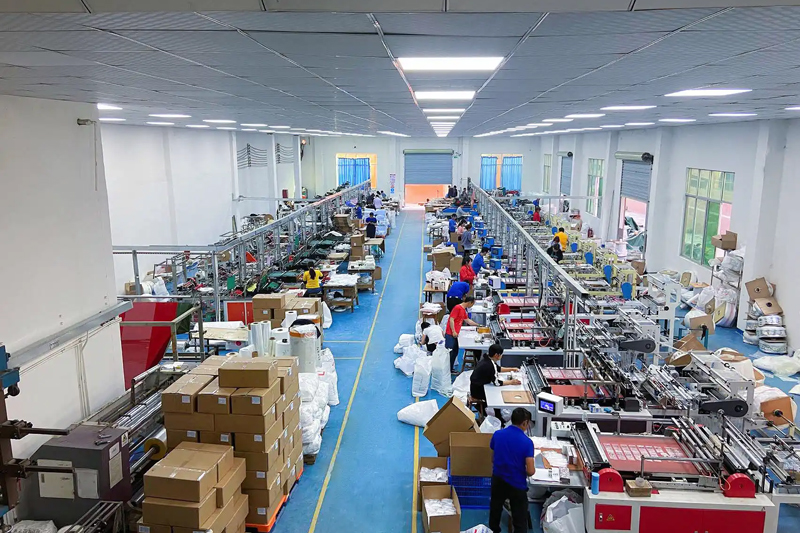
Manufacturing food-contact packaging requires clinical manufacturing environments. At Shandong Jike International Trade Co., Ltd., state-owned automated manufacturing standards guarantee absolute hygienic compliance across every manufacturing phase:

  • Cleanroom Lamination & Solventless Adhesive: Employing advanced non-solvent laminating machines to prevent residual aromatic hydrocarbon retention, ensuring odorless, compliant contact layers.
  • Precision High-Speed Gravure Presses: Electronic shaft gravure printing systems running up to 350 meters/minute with automatic computerized vision inspection to eliminate register misalignment and color deviation (ΔE < 1.5).
  • Hermetic Seal Integrity & Burst Testing: Tensile and burst pressure tests ensure 8-side seal and quad-seal bags withstand air freight pressure differentials without risk of catastrophic package rupture.
  • Comprehensive Global Food Certifications: Fully audited and certified under ISO9001 quality, ISO14001 environmental, ISO45001 safety, and national QS food-grade manufacturing authorizations.
2003 Established Pioneer
8,000+ Annual Tons Capacity
100+ Packaging Engineers
500+ Global Enterprise Brands
70+ Countries Exported

Complete Food Grade Packaging Product Series

Explore our comprehensive portfolio of FDA-compliant, multi-layer custom branded bags and films available for global wholesale manufacturing.

Custom Printed Coffee Bags with Aroma Valve

Multi-layer food-grade laminated coffee pouch with one-way degassing valve and tamper-evident pull-tab zipper.

View Product →

Stand Up Spout Pouch for Liquid & Purees

Custom reusable liquid doypack fitted with high-flow spout for beverage, sauces, and culinary dressings.

View Product →

Custom Grain & Rice Storage Barrier Pouch

Heavy-duty food-grade grain packaging bag offering puncture resistance, humidity defense, and sturdy shelf stability.

View Product →

Wholesale Stand-Up Pouch With Valve

Precision volume range (100ml to 500ml) food packaging pouch designed for liquids, concentrates, and pastes.

View Product →

Flat Bottom Pet Food & Snack Mylar Bag

Heavyweight 2.5kg-20kg box-pouch profile engineered with resealable closure and odor-blocking composite foil walls.

View Product →

Custom Liquid Sauce Dispensing Spout Pouch

High-speed hot-fill compatible pouch suited for ketchup, barbecue sauces, syrups, and edible oils with zero leakage.

View Product →

Sealed Juice & Beverage Pouch with Straw Nozzle

Crystal clear or high-opacity printed plastic packaging with sealed spout neck for on-the-go fruit drinks and hydration products.

View Product →

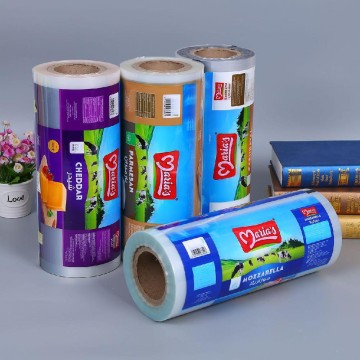
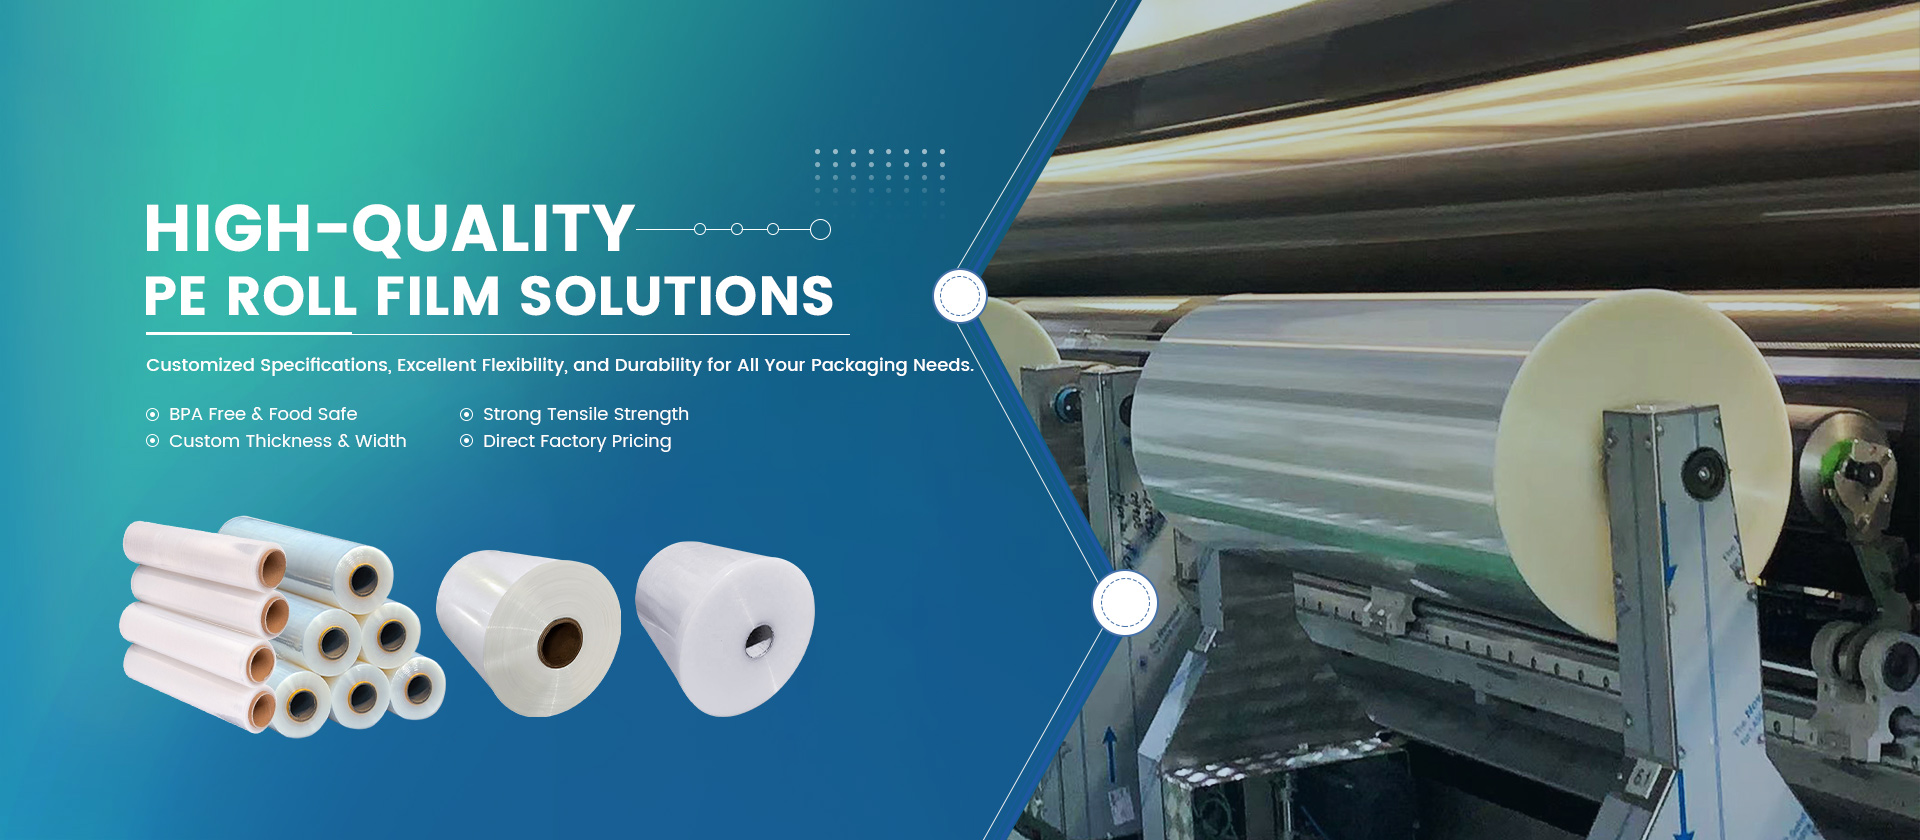
Laminated Aluminum Foil Roll Film & Sachet Rolls

High-speed Form-Fill-Seal (FFS) rollstock film engineered for potato chips, confectionery, nutritional supplements, and single-serve sachets.

View Product →

Ready to Engineer Your Retail-Ready Printed Food Packaging?

Partner with Shandong Jike International Trade Co., Ltd. for fully certified food-grade materials, precision multi-color printing, custom thickness engineering, and direct door-to-door global fulfillment.

Request Custom Quotation & Samples