Welcome to our company
Leave Your Message
High-performance food grade packaging bags engineered for long-term vacuum food storage — custom printed, barrier-sealed, and globally certified.
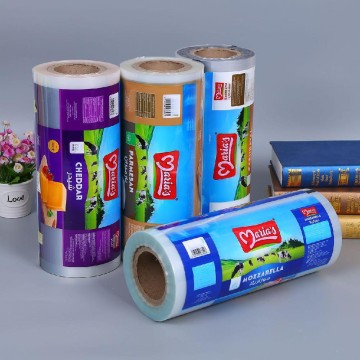
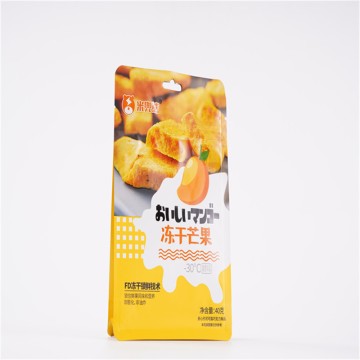
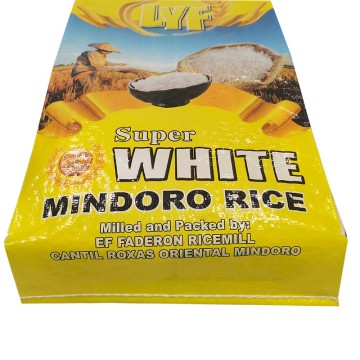
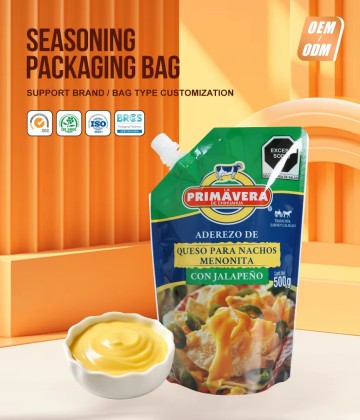
An in-depth look at the commercial landscape, industrial applications, and future trajectory of vacuum food storage packaging.
The global demand for food grade packaging bags designed for long-term vacuum food storage has surged dramatically over the past decade. Driven by shifting consumer behaviors, expanding e-commerce food markets, stricter food safety regulations, and the need to reduce food waste across supply chains, vacuum packaging has evolved from a niche industrial process into a mainstream necessity for food manufacturers, retailers, and households worldwide.
According to recent market intelligence reports, the global flexible food packaging market is projected to exceed USD 280 billion by 2028, with vacuum packaging bags representing one of the fastest-growing segments. Key commercial drivers include:
Modern food grade vacuum packaging bags are engineered using multi-layer co-extrusion or lamination technology, combining materials such as:
The oxygen transmission rate (OTR) of premium vacuum bags can be as low as 0.5–1.0 cc/m²/day, while moisture vapor transmission rate (MVTR) reaches below 1.0 g/m²/day — parameters that directly determine the shelf life extension capability of the packaging.
Advanced production facilities now deploy AI-assisted quality inspection systems, automated gravure printing presses with 10-color capability, and inline leak detection equipment to ensure every bag meets food-grade compliance standards including FDA 21 CFR, EU Regulation 10/2011, and China GB 9683.
The vacuum packaging industry is undergoing a profound transformation as sustainability mandates tighten globally. Key trends include:
Vacuum packaging is the gold standard for extending the shelf life of fresh and processed meats. High-barrier nylon/PE bags reduce microbial growth by removing oxygen, extending beef shelf life from 5 days (unwrapped) to 35–45 days under refrigeration. For seafood exporters, vacuum-sealed bags combined with MAP (modified atmosphere packaging) technology enable transcontinental shipping without quality degradation.
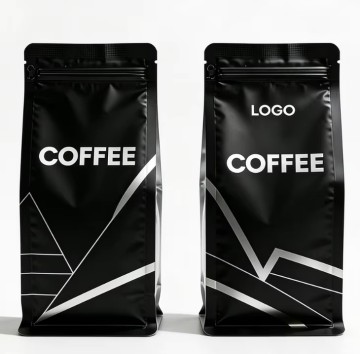
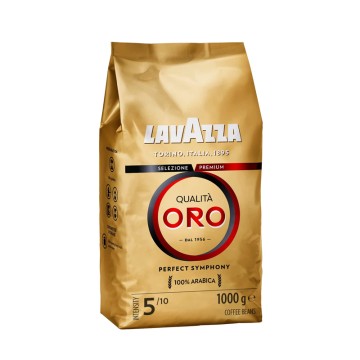
Roasted coffee beans are among the most oxygen-sensitive food products. Food grade vacuum bags with integrated one-way degassing valves allow CO₂ to escape post-roasting while preventing oxygen ingress — preserving aroma compounds for 12–18 months. Specialty coffee roasters worldwide now specify 8-side-seal flat bottom bags with zipper closures as the premium presentation format.
For bulk commodity storage, laminated woven polypropylene vacuum bags in 5kg, 10kg, and 25kg formats provide cost-effective moisture and pest protection for rice, wheat, corn, and seeds. Industrial vacuum packing systems can process thousands of bags per hour, making this a critical component of national food security infrastructure in Asia, Africa, and the Middle East.
The crossover between food packaging and pharmaceutical packaging is growing. Vacuum bags for protein powders, vitamin supplements, and herbal products must meet both food-grade and pharmaceutical-grade standards, often requiring foil-laminated structures with child-resistant closures and tamper-evident seals.
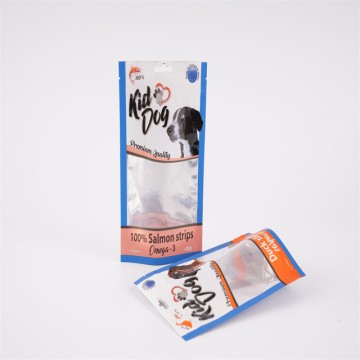
Premium pet food brands are increasingly adopting the same high-barrier vacuum packaging standards used for human food. Resealable stand-up pouches with octagonal seals and zipper closures maintain product freshness between servings while providing a premium shelf presentation that commands higher retail price points.
The sous vide cooking method — which involves vacuum-sealing food and cooking it at precisely controlled temperatures — demands packaging that can withstand temperatures up to 90°C without delamination or seal failure. Retort-grade vacuum pouches enable manufacturers to produce shelf-stable ready meals with 12–24 month ambient shelf lives without preservatives.
Multi-layer PET/AL/PE laminate structures with OTR as low as 0.5 cc/m²/day — locking out oxygen, moisture, and UV light to maximize shelf life in long-term vacuum storage applications.
All materials comply with FDA 21 CFR, EU Regulation 10/2011, and China GB standards. ISO9001, ISO14001, and ISO45001 certified production with QS food safety approval on every product line.
Up to 10-color high-definition gravure printing with support for multi-language labels, barcodes, QR codes, and brand-specific structural designs. MOQ flexibility for both small-batch and large-volume orders.
Mono-material recyclable structures, biodegradable PLA-blend films, and reduced-gauge downgauged options available — meeting EU Green Deal packaging requirements and brand sustainability commitments.
Products pre-engineered to meet the regulatory and labeling requirements of North America, EU, Southeast Asia, Middle East, and beyond. Multilingual packaging design support included.
AI-assisted inline inspection, automated leak detection, and standardized production workflows ensure consistent quality across every batch — from 1,000 units to multi-million unit orders.
Understanding where the industry is heading helps buyers and brands make smarter packaging decisions today.
NFC chips and freshness-indicating sensors embedded in vacuum bags enable real-time shelf life monitoring, cold-chain verification, and direct-to-consumer engagement via smartphone scanning.
Industry-wide shift toward all-PE and all-PP structures that maintain high-barrier performance while enabling recycling through standard household and industrial streams.
Oxygen scavengers, moisture absorbers, and antimicrobial agents incorporated directly into bag structures — extending shelf life beyond what passive barrier films alone can achieve.
SiOx and AlOx nano-coatings applied to film surfaces deliver glass-like oxygen barrier properties with 20–30% less material — reducing cost, weight, and environmental footprint simultaneously.
Growing demand for vacuum pouches that survive sterilization processes up to 121°C, enabling shelf-stable ready meals without preservatives — a key trend in Asia-Pacific and military supply chains.
Digital printing technology eliminates plate costs, enabling brands to produce small-batch, regionally customized, or seasonally limited vacuum packaging runs with fast turnaround times.
From farm to fork — food grade vacuum bags serve critical roles across the entire food production and distribution ecosystem.
High-barrier nylon/PE vacuum bags extend refrigerated shelf life of fresh meats from 5 days to 35–45 days. Essential for export-grade seafood packaging requiring transcontinental cold-chain integrity.
One-way valve vacuum bags preserve roasted coffee aroma for 12–18 months. 8-side-seal flat bottom formats with zipper closures are the premium standard for specialty coffee brands globally.
Laminated PP woven vacuum sacks in 5–25kg formats provide cost-effective long-term storage for rice, wheat, corn, and seeds — critical for food security programs across Asia, Africa, and the Middle East.
Resealable stand-up zipper pouches with octagonal seals bring human-food-grade barrier protection to premium pet food products, extending freshness between servings and enhancing shelf appeal.
Retort-grade vacuum pouches withstand sterilization at 121°C, enabling preservative-free shelf-stable ready meals with 12–24 month ambient shelf lives — a rapidly growing segment globally.
Foil-laminated vacuum bags for protein powders, vitamins, and herbal supplements meet dual food-grade and pharmaceutical-grade standards with tamper-evident seals and child-resistant closures.
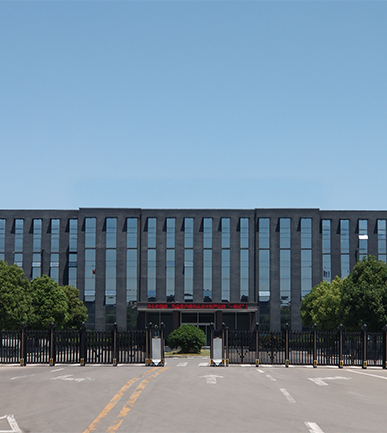
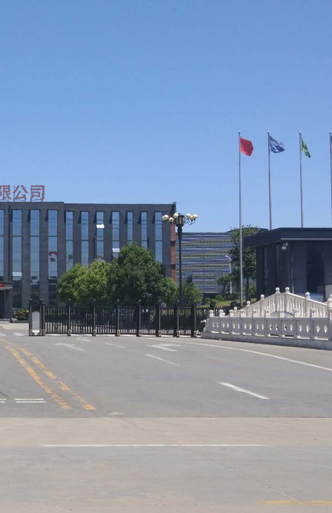
Shandong Jike International Trade Co., Ltd. is a state-owned professional food packaging and printing enterprise, established in 2003 and located in Shandong Province, eastern China. The company has obtained and passed ISO9001, ISO14001, and ISO45001 certifications, and all our products have passed QS food safety certification.
With over two decades of expertise in food grade flexible packaging manufacturing, we have built a reputation for delivering precision-engineered vacuum packaging solutions that meet the most demanding international food safety and regulatory standards.
Trusted by food manufacturers, brand owners, and trading companies across more than 70 countries worldwide.
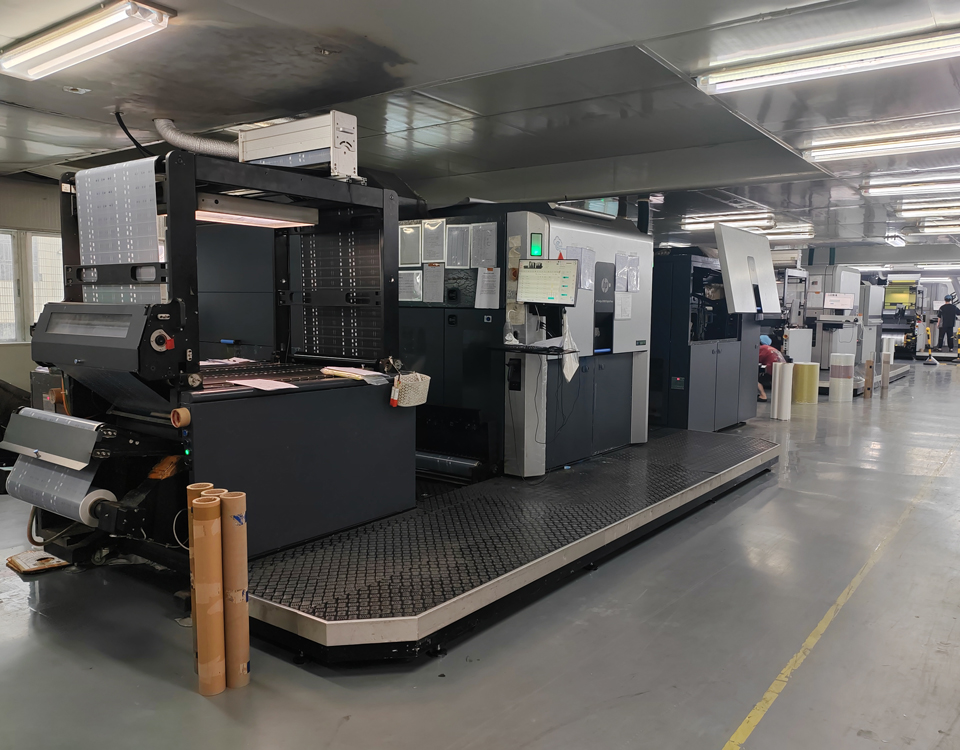
The company's core export products cover the needs of multiple industries, mainly including food-grade flexible packaging, pet food packaging, polyethylene film, and woven packaging bags, which can accurately match the market standards of different regions such as North America, the European Union, Southeast Asia, and the Middle East.
We also support multi-language design and printing, barcode/QR code customization, material combination selection, and thickness selection to fully meet the needs of cross-border trade. Every product is engineered with long-term vacuum food storage performance as the primary design criterion.
In terms of supply chain and service, the company has strong cross-border delivery capabilities. We have standardized production workshops and automated production lines, with flexible minimum order quantities for regular products. We undertake both small-batch customization and large-volume order production.
We have established a strict quality control system, tracing the entire process from raw material procurement and production processing to finished product inspection, ensuring that every batch of products meets the quality standards of the importing country. We are equipped with a professional cross-border logistics team to support various transportation methods such as full container shipping, LCL shipping, and air freight.
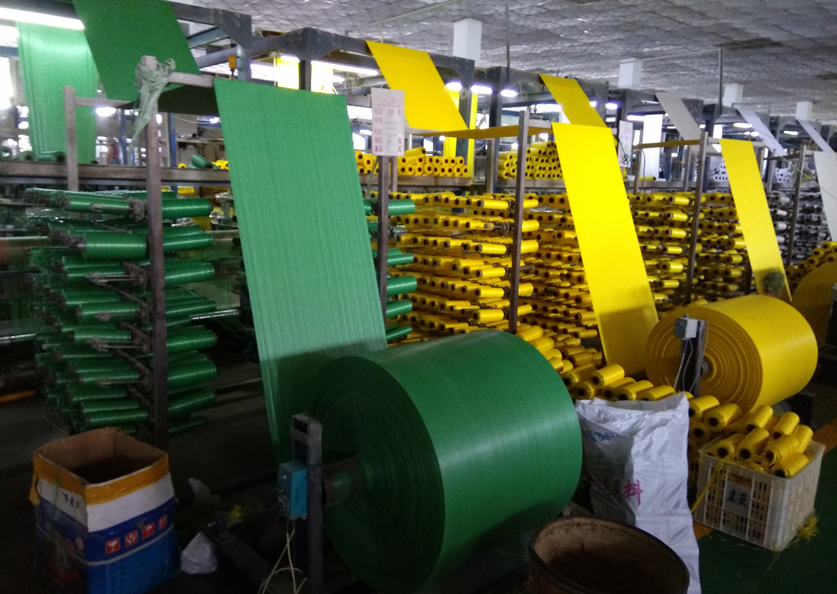
Since its establishment 23 years ago, relying on excellent product quality, comprehensive compliance guarantees, and efficient cross-border services, Jike Packaging Printing has established long-term cooperative relationships with customers in more than 50 countries and regions worldwide, serving clients including globally renowned food manufacturers, brand owners, and trading companies. In the future, we will continue to focus on changes in international market demand, using innovative technology and high-quality services as a link to become a trusted cross-border flexible packaging printing partner for global customers.
Jike Packaging actively participates in major international food packaging exhibitions, showcasing our latest innovations in vacuum food storage packaging technology.
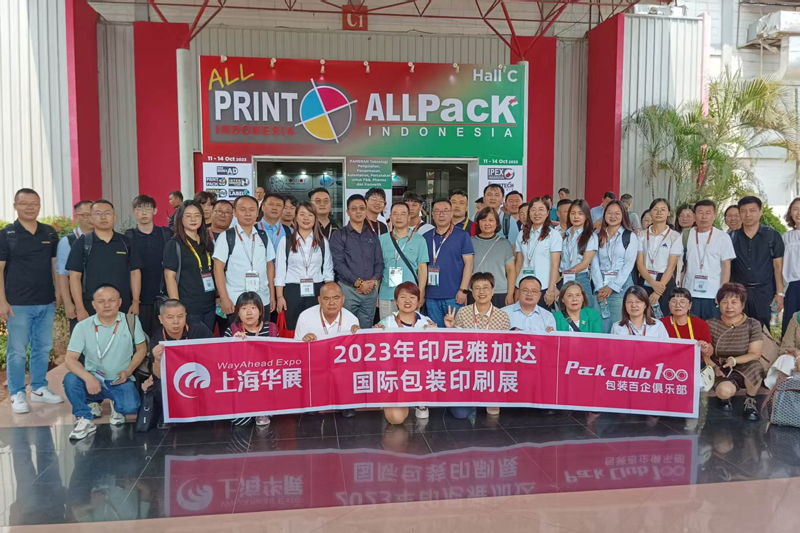
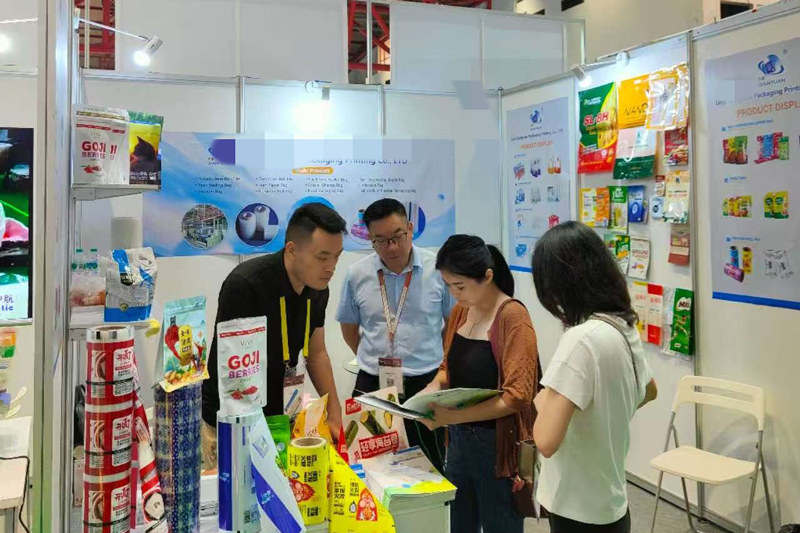
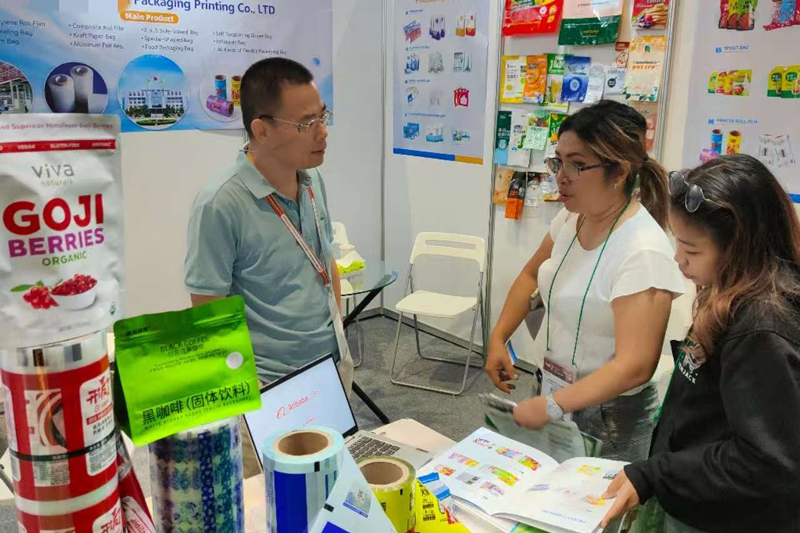
Explore our full product portfolio — all engineered for long-term vacuum food storage with food grade materials and custom printing capabilities.